Với hơn 10 năm kinh nghiệm về vận chuyển khí nén, Headpowder Sơn Đông cung cấp hệ thống, thiết bị và quạt gió toàn chuỗi, đảm nhận các dự án kỹ thuật bột trọn gói trên toàn quốc.
Distillers grains, a byproduct of the ethanol production process, require efficient and reliable transportation systems to move them from processing facilities to storage or further processing. The choice of conveying method significantly impacts operational efficiency, cost, and environmental impact. This article provides a detailed comparison of common distillers grains conveying methods, highlighting their advantages and disadvantages.
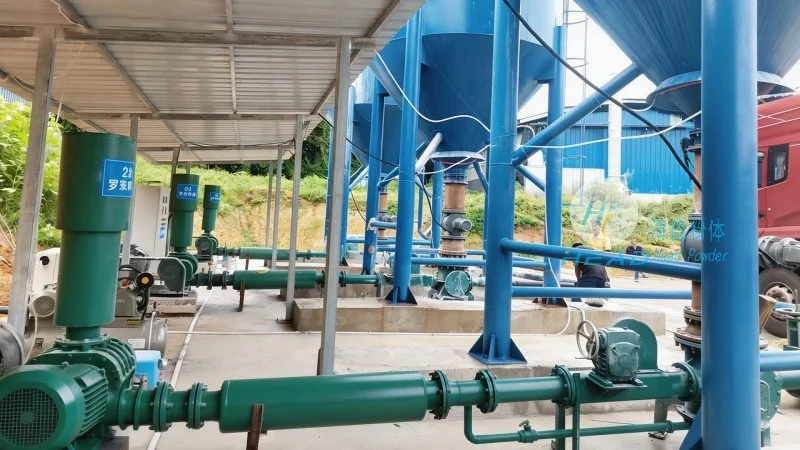
Screw Conveyors for Distillers Grains
Screw conveyors, also known as auger conveyors, are a popular choice for transporting distillers grains due to their compact design and ability to handle a wide range of materials. These systems consist of a rotating helical screw inside a U-shaped trough, which moves material forward through the conveyor. The primary advantages of screw conveyors include their simplicity, low maintenance requirements, and ability to operate in vertical or horizontal configurations. They are particularly effective for handling granular or powdery materials like distillers grains, as the screw provides consistent, low-velocity movement that minimizes material degradation. However, screw conveyors have limitations, such as their inability to handle high volumes of wet or sticky materials, which can lead to clogging and reduced efficiency. Additionally, the friction between the screw and the material can generate heat, potentially affecting the quality of the distillers grains if the material is heat-sensitive.
Belt Conveyors for Distillers Grains
Belt conveyors are another widely used method for transporting distillers grains, especially in applications requiring long-distance or high-volume material movement. These systems utilize a continuous belt looped over rollers, with the material placed on the belt and carried to the destination. The main advantages of belt conveyors include their high capacity, ability to handle large quantities of material, and suitability for long horizontal or inclined runs. They are also relatively simple to install and maintain, with minimal moving parts compared to other systems. However, belt conveyors have drawbacks, such as the risk of material spillage or damage to the belt if the grains are too heavy or abrasive. The belts can also be susceptible to wear and tear from the abrasive nature of distillers grains, requiring regular replacement to maintain efficiency. Furthermore, belt conveyors may not be as effective for vertical lifting as screw conveyors, as the belt's tension and friction can limit the height of the lift.
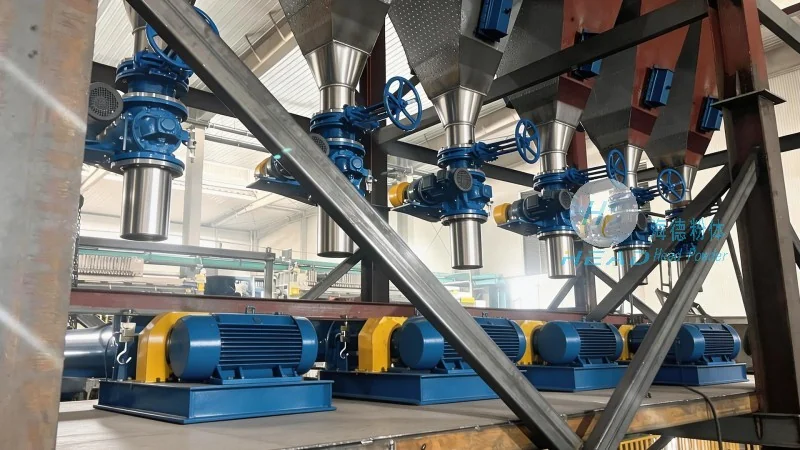
Air-Flow Conveying Systems for Distillers Grains
Air-flow or pneumatic conveying systems use air pressure to transport distillers grains through a pipeline. These systems are particularly useful for applications where dust control is a priority or where the material needs to be moved over long distances without the need for multiple transfer points. The primary advantages of air-flow conveyors include their ability to handle fine or powdery materials without the need for mechanical contact, reducing the risk of material degradation or contamination. They also offer flexibility in terms of layout, as the pipeline can be routed around obstacles or through different levels of a facility. However, air-flow systems have significant disadvantages, including higher energy consumption compared to mechanical conveyors, as they require powerful blowers to generate the necessary air pressure. The cost of the system is also higher due to the need for specialized equipment like cyclones and filters to separate the material from the air. Additionally, air-flow conveyors may not be suitable for handling wet or sticky distillers grains, as the material can clog the pipeline or reduce the efficiency of the system.
HeadPowder's Expertise in Distillers Grains Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. specializes in providing customized conveying solutions tailored to the unique needs of distillers and ethanol producers. With years of experience in the industry, HeadPowder understands the challenges associated with transporting distillers grains and offers a range of equipment and services to optimize operational efficiency. The company's team of engineers and technicians work closely with clients to assess their specific requirements, such as material characteristics, volume, and distance, to recommend the most suitable conveying method. HeadPowder's products include high-quality screw conveyors, belt conveyors, and air-flow systems, all designed to meet the rigorous demands of the ethanol industry. The company also provides maintenance and support services to ensure that the conveying systems operate at peak performance, minimizing downtime and maximizing productivity. By choosing HeadPowder, distillers can benefit from reliable, efficient, and cost-effective conveying solutions that enhance their overall operational performance.
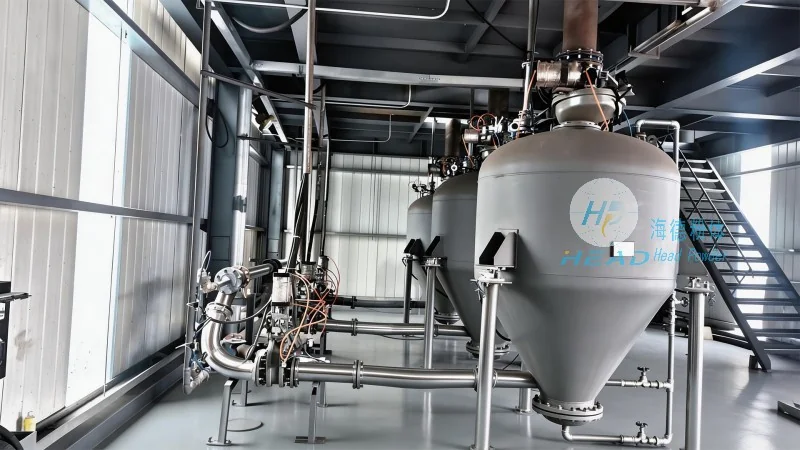
Conclusion
Choosing the right distillers grains conveying method is a critical decision for any ethanol producer, as it directly impacts operational efficiency, cost, and product quality. While each method has its advantages and disadvantages, the optimal choice depends on the specific application and material characteristics. Screw conveyors are ideal for short-distance, low-volume applications, while belt conveyors are better suited for long-distance, high-volume movement. Air-flow systems offer flexibility and dust control but require higher energy input. Shandong HeadPowder Engineering Co., Ltd. provides expert guidance and customized solutions to help distillers select the most appropriate conveying method for their needs, ensuring efficient and reliable transportation of distillers grains. By partnering with HeadPowder, distillers can enhance their operational performance and achieve better results in their ethanol production processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu