Với hơn 10 năm kinh nghiệm về vận chuyển khí nén, Headpowder Sơn Đông cung cấp hệ thống, thiết bị và quạt gió toàn chuỗi, đảm nhận các dự án kỹ thuật bột trọn gói trên toàn quốc.
For industrial facilities handling nitrate ammonium, selecting an appropriate pneumatic conveying system is crucial to ensure efficient, safe, and cost-effective material transport. The choice of system directly impacts operational performance, maintenance requirements, and overall process reliability. This guide outlines key considerations and factors to help you select the optimal pneumatic conveying system tailored to your nitrate ammonium transport needs.
Understanding the Importance of Pneumatic Conveying for Nitrate Ammonium
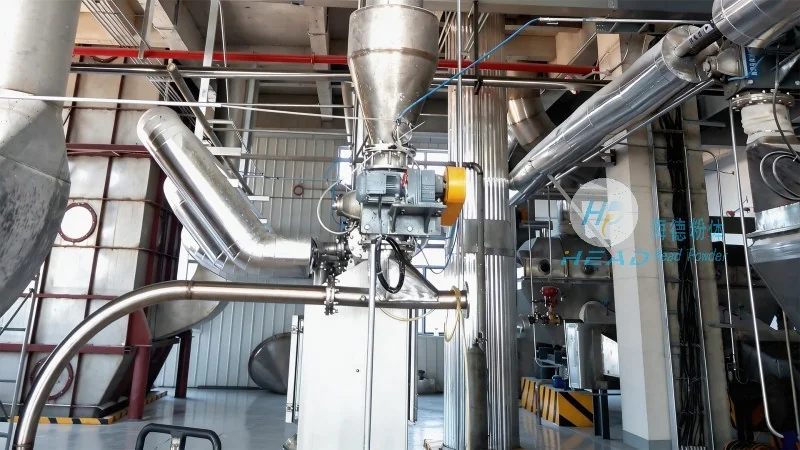
Nitrate ammonium is a critical chemical used in various industries, including fertilizers, explosives, and chemical manufacturing. Its handling requires specialized equipment due to its properties, such as particle size, moisture content, and potential reactivity. Pneumatic conveying systems offer a flexible and effective solution for transporting this material from storage to processing units, or between different stages of production. Unlike traditional mechanical conveying methods, pneumatic systems use air or gas to move material through pipelines, reducing the risk of contamination and minimizing the need for physical contact with the material.
About HeadPowder: Your Partner in Pneumatic Conveying Solutions
HeadPowder, a leading provider of engineering solutions, specializes in designing and manufacturing pneumatic conveying systems for diverse industrial applications. With a strong presence in Shandong, China, HeadPowder combines years of experience and advanced technology to deliver customized solutions that meet the unique requirements of each client. The company’s commitment to quality, safety, and efficiency has made it a trusted name in the industry, serving a wide range of sectors including chemical, food, and pharmaceuticals.
Types of Pneumatic Conveying Systems for Nitrate Ammonium
When selecting a pneumatic conveying system for nitrate ammonium, it is essential to consider the specific characteristics of the material and the operational conditions. Two primary types of systems are commonly used: positive pressure and negative pressure (or vacuum) systems.
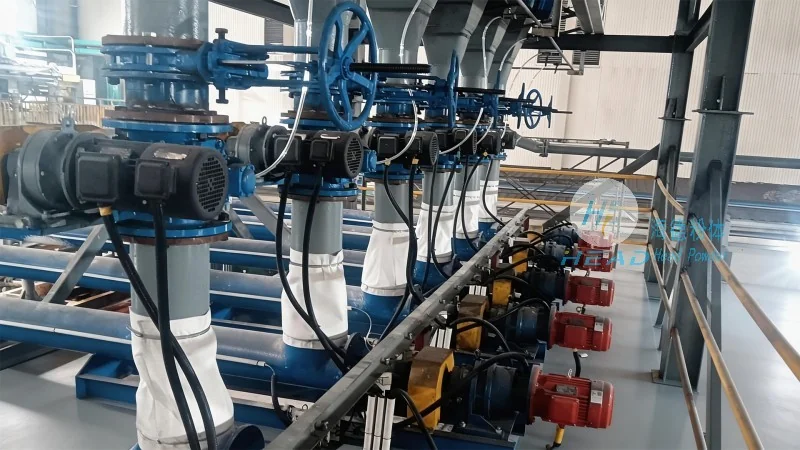
Positive pressure systems, also known as pressure conveying, operate by blowing air or gas into the conveying line, pushing the material forward. This method is ideal for applications requiring high material flow rates and long-distance transport. It is particularly suitable for nitrate ammonium with relatively dry and free-flowing particles, as it minimizes the risk of material degradation and blockages. Positive pressure systems often use rotary air locks, cyclones, and other components to control the flow and separation of material.
Negative pressure systems, or vacuum conveying, work by creating a vacuum in the conveying line, drawing material from the source into the system. This approach is well-suited for applications where the material needs to be transported from multiple points or where the source is at a higher elevation. Vacuum systems are effective for handling fine or dusty materials, as they can maintain a clean and controlled environment. However, they may require more maintenance and are generally less efficient for long-distance transport compared to positive pressure systems.
Key Factors to Consider When Choosing a Pneumatic Conveying System
Choosing the right pneumatic conveying system for nitrate ammonium involves evaluating several critical factors to ensure optimal performance and alignment with your process requirements.
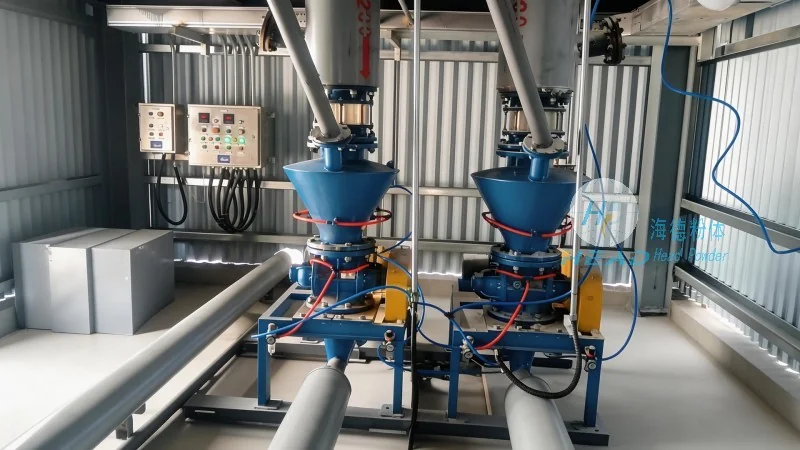
First, the material characteristics of nitrate ammonium must be carefully analyzed. Factors such as particle size distribution, moisture content, and bulk density influence the system’s design. For example, if the material is fine and prone to dust, a system with effective filtration and dust control measures is essential to prevent contamination and ensure compliance with safety regulations. Additionally, the material’s reactivity and potential for caking or agglomeration must be considered, as these can impact the system’s efficiency and require specialized equipment like agitators or vibrators.
Second, the operational parameters of your process are crucial. The required flow rate, conveying distance, and system pressure or vacuum levels need to be determined based on the production scale and throughput. For high-volume operations, a positive pressure system with a larger blower capacity may be necessary to maintain consistent material flow. Conversely, for smaller-scale applications or when transporting material over shorter distances, a negative pressure system may be more cost-effective.
Third, the integration of the system with existing infrastructure is another important consideration. The existing layout of the facility, including the location of storage tanks, processing units, and waste disposal areas, will dictate the pipeline design and system configuration. A well-designed system should minimize the need for extensive modifications to the plant, reducing installation time and costs. Additionally, the system’s compatibility with other equipment, such as feeders, mixers, and control systems, must be ensured to maintain seamless operation.
Fourth, safety and regulatory compliance are paramount when handling nitrate ammonium. Pneumatic conveying systems must adhere to local and international safety standards to prevent accidents and ensure the well-being of personnel. This includes features like explosion-proof components, proper ventilation, and emergency shutdown mechanisms. HeadPowder’s systems are designed with safety in mind, incorporating advanced controls and monitoring systems to detect and mitigate potential hazards.
Fifth, maintenance and operational costs should be evaluated to ensure long-term cost-effectiveness. While initial investment may vary between system types, the total cost of ownership, including maintenance, energy consumption, and downtime, should be considered. Systems with lower maintenance requirements and higher energy efficiency can provide significant savings over time. HeadPowder offers systems with modular components that are easy to maintain and replace, reducing downtime and extending the system’s lifespan.
Customization and Support from HeadPowder
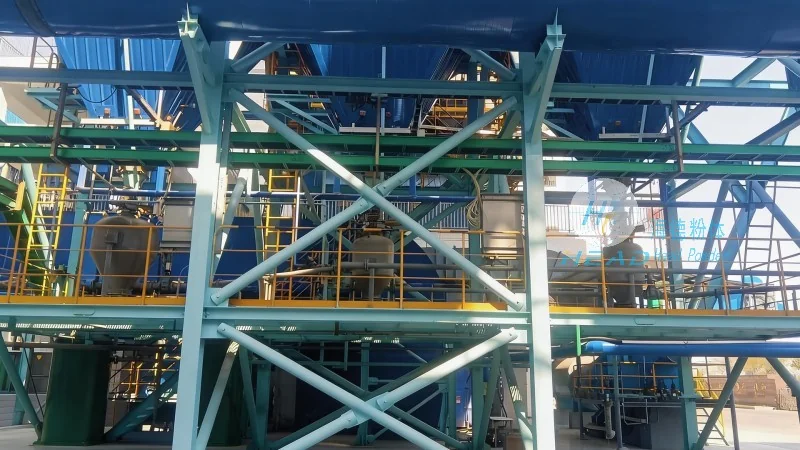
HeadPowder understands that each nitrate ammonium transport process is unique, and a one-size-fits-all solution is not always optimal. The company provides comprehensive engineering services to customize pneumatic conveying systems that meet the specific needs of each client. From initial consultation and system design to installation and commissioning, HeadPowder’s team of experts works closely with clients to develop tailored solutions.
HeadPowder’s engineers conduct thorough assessments of the material properties, process requirements, and site conditions to design a system that maximizes efficiency and minimizes risks. The company uses advanced software and simulation tools to model the system’s performance, ensuring that the final design meets all operational and safety criteria. This approach allows for early identification and resolution of potential issues, reducing the likelihood of costly modifications during the installation phase.
Post-installation support is also a key aspect of HeadPowder’s service. The company provides training for plant operators on system operation and maintenance, ensuring that the equipment is used effectively and efficiently. Additionally, HeadPowder offers ongoing technical support and maintenance services to address any issues that may arise during the system’s operation. This commitment to customer support helps to maximize the system’s performance and extend its lifespan, providing long-term value to clients.
Conclusion: Selecting the Right Pneumatic Conveying System for Nitrate Ammonium
Choosing the right pneumatic conveying system for nitrate ammonium is a critical decision that impacts the efficiency, safety, and cost-effectiveness of your industrial operations. By considering the material characteristics, operational parameters, integration with existing infrastructure, safety requirements, and maintenance costs, you can select a system that meets your specific needs. HeadPowder, with its expertise and customized solutions, is a reliable partner in this process, helping you achieve optimal performance and reliability in your nitrate ammonium transport processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu