Với hơn 10 năm kinh nghiệm về vận chuyển khí nén, Headpowder Sơn Đông cung cấp hệ thống, thiết bị và quạt gió toàn chuỗi, đảm nhận các dự án kỹ thuật bột trọn gói trên toàn quốc.
Sodium stearate, a widely used chemical compound, is often required to be transported efficiently from production sites to various application areas. The choice of delivery method significantly impacts operational efficiency, cost-effectiveness, and product quality. This article explores the primary delivery methods for sodium stearate, with a particular focus on the advantages and features of air-driven conveying systems.
Common Delivery Methods for Sodium Stearate
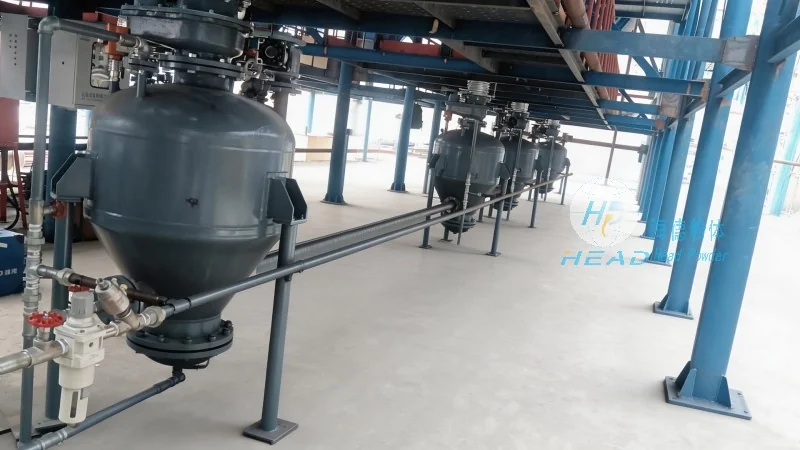
Traditionally, sodium stearate has been transported using several methods, including bulk containers, conveyor belts, and pneumatic conveying systems. Bulk containers such as trucks or railcars are commonly used for long-distance transportation, but they may face challenges with dust control and material handling. Conveyor belts, while effective for horizontal or slight incline transport, are limited by the physical properties of the material and may require additional equipment for vertical movement. Pneumatic conveying, particularly air-driven systems, has emerged as a preferred solution for many industries due to its versatility and efficiency.
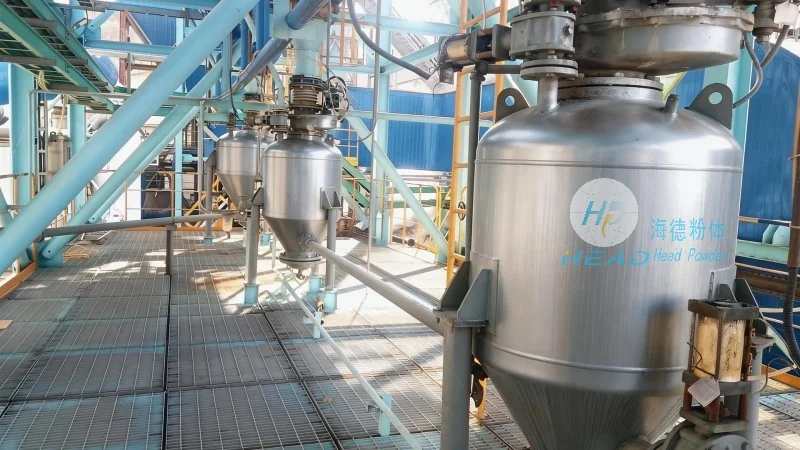
Advantages of Air-Driven Conveying for Sodium Stearate
When considering the advantages of air-driven conveying for sodium stearate, several key benefits stand out. First, air conveying systems provide a dust-free environment, which is crucial for maintaining product purity and meeting stringent quality standards. Unlike traditional methods that may generate dust during loading or unloading, pneumatic systems keep the material contained within the conveying line, reducing contamination risks. Second, air-driven conveyors offer high throughput rates, allowing for rapid and continuous material transfer. This is particularly beneficial in high-volume production environments where downtime can be costly. Third, these systems are highly flexible, capable of transporting materials over long distances and through complex layouts, including vertical lifts and multiple transfer points. The ability to integrate with existing production lines also enhances operational efficiency.
Key Features of Air Conveying Systems for Sodium Stearate
Several features make air-driven conveying systems ideal for sodium stearate applications. One of the most notable is the ability to handle fine powders and granules without causing agglomeration or degradation. The controlled air flow ensures that the material moves smoothly through the system, preserving its physical properties. Additionally, these systems are designed for minimal maintenance, with components that are easy to inspect and replace, reducing operational downtime. The modular design of air conveyors allows for scalability, enabling companies to expand their conveying capabilities as production needs grow. This adaptability is a significant advantage for businesses operating in dynamic market conditions.
Application Scenarios and Operational Considerations
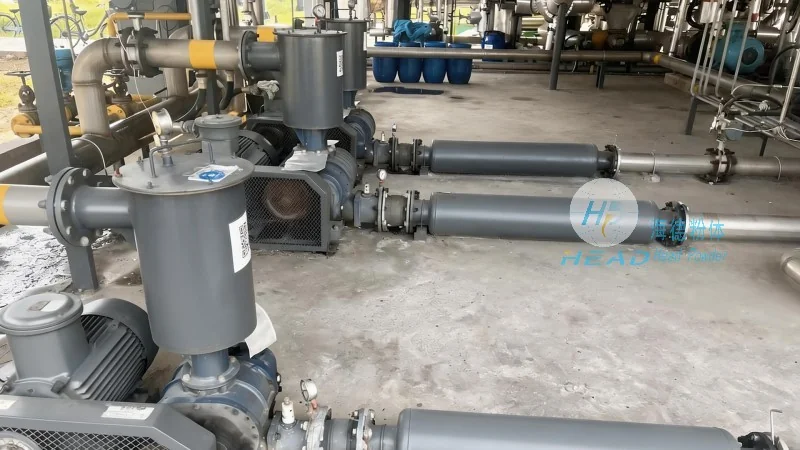
The effectiveness of air-driven conveying for sodium stearate depends on several operational factors. The distance between the source and destination, the volume of material to be transported, and the required speed of delivery all influence the choice of system configuration. For short distances, a simple venturi system may suffice, while longer distances or complex layouts may require more advanced systems such as rotary airlock feeders and positive displacement blowers. Proper system sizing is critical to ensure optimal performance and energy efficiency. Additionally, the material's moisture content and particle size distribution must be considered, as these factors affect the air flow requirements and system design. Regular maintenance, including filter cleaning and air pressure checks, is essential to maintain system efficiency and prevent material buildup.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and installation of advanced material handling systems. With a focus on providing customized solutions for various industrial applications, the company has established itself as a leader in the field of pneumatic conveying technology. Headpowder's expertise lies in developing efficient and reliable systems that meet the specific needs of clients, ensuring optimal performance and cost savings. The company's commitment to quality and innovation has enabled it to serve a wide range of industries, including chemical, food, and pharmaceutical sectors. Headpowder's facilities are located in Shandong, China, where the company leverages local resources and expertise to deliver high-quality products and services to its global clientele.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu