Với hơn 10 năm kinh nghiệm về vận chuyển khí nén, Headpowder Sơn Đông cung cấp hệ thống, thiết bị và quạt gió toàn chuỗi, đảm nhận các dự án kỹ thuật bột trọn gói trên toàn quốc.
When it comes to efficiently handling corn cob material in agricultural and industrial settings, selecting the right conveying method is crucial. The choice of equipment directly impacts productivity, cost-effectiveness, and operational safety. This article provides a detailed comparison of common corn cob conveying methods, focusing on their advantages and disadvantages, to help businesses make informed decisions.
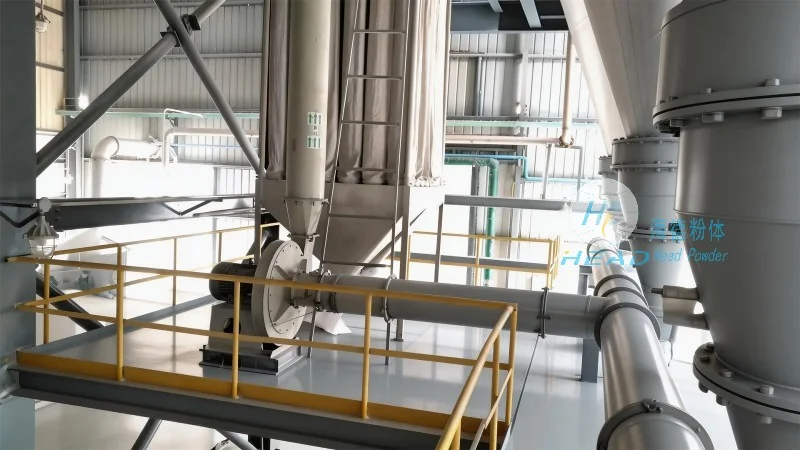
Introduction to Corn Cob Conveying Systems
Corn cob, a byproduct of corn processing, is widely used in animal feed, biofuel production, and other industrial applications. Efficient transportation of corn cob from storage to processing units is essential for maintaining smooth operations. Various conveying systems are available, each with unique characteristics suited to different operational needs.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer of specialized conveying equipment, has been serving the agricultural and industrial sectors for years. With a strong presence in Shandong, China, the company specializes in designing and manufacturing high-quality corn cob conveying solutions tailored to client requirements. Their expertise in material handling ensures reliable performance and durability in demanding environments.
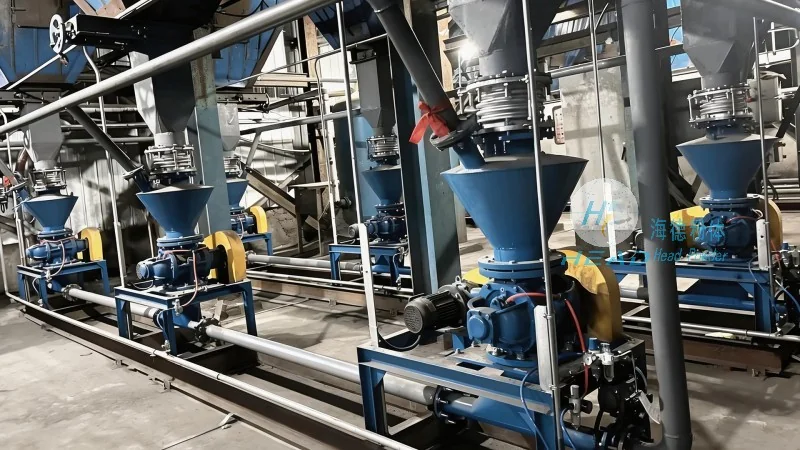
1. Screw Conveyor (Auger Conveyor)
Screw conveyors, also known as auger conveyors, are among the most common methods for transporting corn cob. These systems consist of a rotating helical screw inside a tube, which moves material forward through the conveyor. The primary advantage of screw conveyors is their simplicity and low maintenance requirements. They are suitable for horizontal or slightly inclined transport and can handle a wide range of bulk materials, including corn cob. However, their limitations include the risk of material bridging and blockages, especially with fibrous materials like corn cob. Additionally, screw conveyors may not be ideal for long-distance transport due to the potential for increased friction and wear on the screw and tube.
2. Pneumatic Conveying System
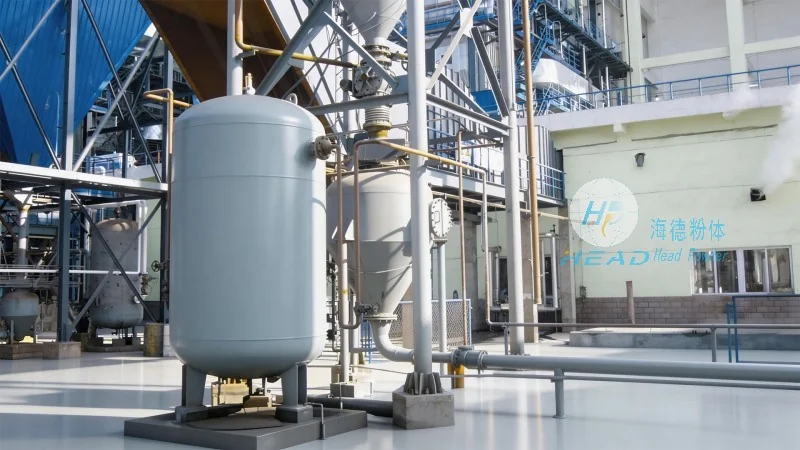
Pneumatic conveying systems use air pressure to transport corn cob through a pipeline. This method is highly effective for both short and long-distance transport, offering flexibility in layout and the ability to handle materials with high moisture content. One of the key advantages of pneumatic conveying is its ability to transport materials in a closed system, reducing dust and contamination. It also allows for the integration of multiple processing units along the conveying line. However, pneumatic systems require higher energy consumption compared to mechanical conveyors, and the initial investment can be substantial. Moreover, they may not be suitable for very fine or abrasive materials, as the air flow can cause wear on the pipeline and components.
3. Belt Conveyor
Belt conveyors are widely used in bulk material handling, including corn cob. These systems consist of a continuous belt that moves over rollers or pulleys, transporting material from one point to another. Belt conveyors are known for their high capacity and ability to handle large volumes of corn cob efficiently. They are suitable for both horizontal and inclined transport and can cover long distances with minimal maintenance. The main advantage of belt conveyors is their durability and reliability, making them ideal for continuous operation in industrial settings. However, they require regular maintenance to ensure proper tension and alignment of the belt. Additionally, belt conveyors may not be suitable for materials with high moisture content or those that are prone to sticking to the belt surface.
4. Bucket Elevator
Bucket elevators are vertical or inclined conveyors that use buckets attached to a chain or belt to lift and transport corn cob. These systems are particularly effective for vertical transport, allowing material to be moved from lower to higher levels with minimal space requirements. The primary advantage of bucket elevators is their high lifting capacity and ability to handle materials with high moisture content or those that are prone to clogging. They are also suitable for transporting materials over long vertical distances. However, bucket elevators have higher initial costs compared to other conveying methods and require more maintenance due to the moving parts and the need for proper bucket alignment. Additionally, they may not be ideal for very fine or lightweight materials, as the buckets may not effectively grip the material.
Conclusion and Recommendations
Choosing the right corn cob conveying method depends on several factors, including the volume of material to be transported, the distance, the layout of the facility, and the specific characteristics of the corn cob. Screw conveyors are suitable for short horizontal transport with low to moderate volumes. Pneumatic systems excel in long-distance or enclosed transport with high material flexibility. Belt conveyors are ideal for high-capacity horizontal transport in industrial settings. Bucket elevators are best for vertical transport with high lifting requirements.
For businesses seeking reliable and efficient corn cob conveying solutions, HeadPowder offers a range of customized systems designed to meet specific operational needs. By considering the advantages and disadvantages of each method, companies can select the most suitable equipment to enhance productivity, reduce costs, and ensure safe operation.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu