Với hơn 10 năm kinh nghiệm về vận chuyển khí nén, Headpowder Sơn Đông cung cấp hệ thống, thiết bị và quạt gió toàn chuỗi, đảm nhận các dự án kỹ thuật bột trọn gói trên toàn quốc.
Coffee powder, as a critical component in the coffee industry, requires efficient and reliable conveying methods to ensure smooth production processes. The choice of transport system significantly impacts product quality, safety, and overall operational efficiency. This article explores various methods used for coffee powder conveying, highlighting the advantages and considerations for each approach.
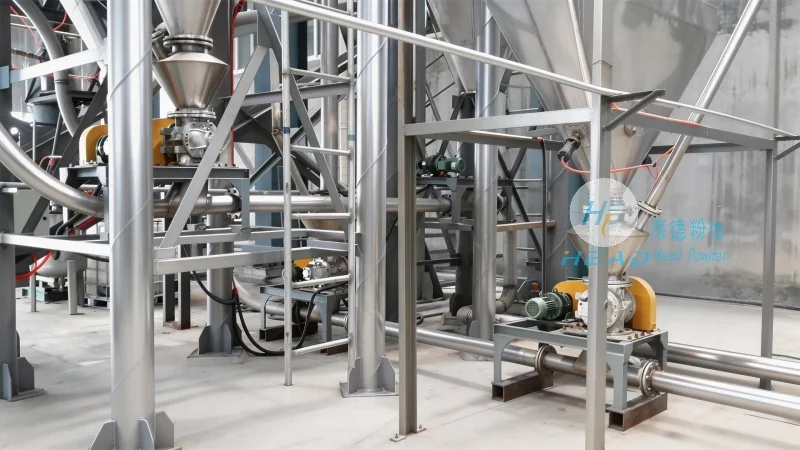
Understanding the Importance of Coffee Powder Conveying
Efficient coffee powder conveying is crucial for maintaining product integrity and preventing contamination. Coffee powder is a fine, dry material that can be prone to caking, bridging, or dust generation if not handled properly. Proper conveying systems help in maintaining consistent moisture levels, preventing agglomeration, and ensuring that the powder moves smoothly from storage to processing equipment. This not only enhances operational efficiency but also contributes to the final quality of coffee products.
Key Factors to Consider When Choosing a Conveying System
Before selecting a coffee powder conveying method, several factors must be evaluated. These include the volume of material to be transported, the distance over which it needs to be moved, the required speed of transfer, and the space constraints within the facility. Additionally, the characteristics of the coffee powder itself—such as particle size, density, and flowability—are critical. Some systems may be better suited for handling fine powders, while others are more effective for bulk materials. The choice of system also depends on the need for minimal product degradation, energy efficiency, and ease of maintenance.
Common Coffee Powder Conveying Methods
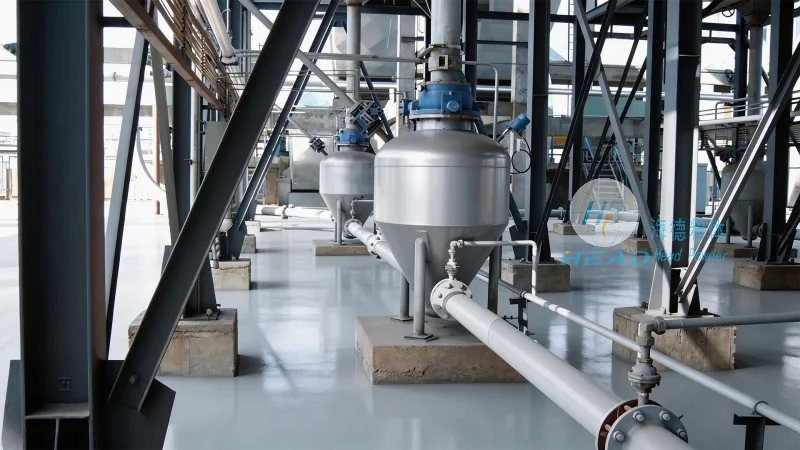
There are several established methods for transporting coffee powder, each with its own set of applications and benefits. The most common approaches include screw conveyors, pneumatic conveying systems, and vibrating conveyors. Each method has unique advantages and is selected based on specific operational requirements.
Screw Conveyors for Coffee Powder Transport
Screw conveyors, also known as auger conveyors, are widely used in the coffee industry for transporting coffee powder. These systems consist of a rotating helical screw inside a tube or trough. As the screw rotates, it pushes the material forward, ensuring a continuous and controlled flow. Screw conveyors are particularly effective for handling fine powders and can be designed to operate at various speeds, allowing for precise control over the conveying rate. They are often used in horizontal or slightly inclined applications, making them suitable for moving coffee powder from storage silos to processing equipment. The enclosed design of screw conveyors helps in minimizing dust dispersion and maintaining product cleanliness. Additionally, these systems are relatively simple in structure, requiring less maintenance compared to more complex pneumatic systems. However, they may not be as efficient for long-distance transport or when dealing with very fine powders that tend to settle or clog the screw.
Pneumatic Conveying Systems for Coffee Powder
Pneumatic conveying systems use air or other gases to transport coffee powder through a pipeline. This method is highly effective for moving fine powders over long distances and can handle both horizontal and vertical transport. There are two main types of pneumatic conveying: pressure and vacuum systems. Pressure systems use compressed air to push the material through the pipeline, while vacuum systems use a vacuum to draw the material. For coffee powder, pressure systems are often preferred as they provide better control over the flow rate and can handle larger volumes. Pneumatic conveying offers several advantages, including the ability to transport materials in a closed system, reducing dust exposure and environmental impact. It also allows for the integration of multiple transfer points and can be easily automated. However, pneumatic systems require more energy compared to mechanical conveyors and may need regular maintenance of air filters and pipeline components to prevent clogging.
Vibrating Conveyors for Coffee Powder Handling
Vibrating conveyors utilize vibrations to move coffee powder along a trough. These systems consist of a conveyor bed that is mounted on springs and driven by an electric motor, which causes the bed to vibrate at a specific frequency. The vibrations help in moving the material forward by creating a series of small steps or cascades. Vibrating conveyors are particularly effective for handling bulk materials with varying particle sizes and can be used in both horizontal and inclined applications. They are often used in coffee processing plants for transporting coffee beans or ground coffee powder from one processing stage to another. The advantage of vibrating conveyors is their ability to handle sticky or cohesive materials without causing blockages, as the vibrations prevent material from sticking to the conveyor surface. However, they may not be as efficient for very fine powders that tend to settle or require high-speed transport.
Other Conveying Options for Coffee Powder
In addition to the primary methods mentioned above, other systems may be used for specific applications. For example, bucket elevators are used for vertical transport of coffee powder, while belt conveyors are suitable for moving larger quantities of material over longer horizontal distances. Each of these systems has its own set of advantages and limitations, and the choice depends on the specific requirements of the coffee processing facility.
Choosing the Right Conveying System for Your Coffee Processing Plant
When selecting a coffee powder conveying system, it is essential to consider the unique needs of your operation. Factors such as the volume of coffee powder to be transported, the distance between processing stages, and the need for minimal product degradation should guide the decision. Additionally, the cost of installation, energy consumption, and maintenance should be evaluated. It is often beneficial to consult with experts in the field, such as Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, to ensure that the chosen system meets all operational requirements and provides long-term efficiency and reliability.
Shandong HeadPowder Engineering Co., Ltd. specializes in providing customized conveying solutions for the coffee industry, including screw conveyors, pneumatic systems, and vibrating conveyors. With years of experience and a deep understanding of coffee processing requirements, the company offers tailored solutions that enhance the efficiency and safety of coffee powder transport. Located in Shandong, China, HeadPowder Engineering Co., Ltd. combines advanced technology with practical expertise to deliver high-quality conveying systems that meet the demands of modern coffee production.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu