Với hơn 10 năm kinh nghiệm về vận chuyển khí nén, Headpowder Sơn Đông cung cấp hệ thống, thiết bị và quạt gió toàn chuỗi, đảm nhận các dự án kỹ thuật bột trọn gói trên toàn quốc.
When it comes to the efficient handling and transportation of barley malt in industrial settings, selecting the right conveying method is crucial for maintaining product quality, operational efficiency, and cost-effectiveness. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. (referred to as HeadPowder) specializes in designing and implementing tailored solutions for malt processing facilities. This article provides a detailed comparison of common barley malt conveying methods, highlighting their respective advantages and disadvantages to help industry professionals make informed decisions.
Overview of Barley Malt Conveying Methods
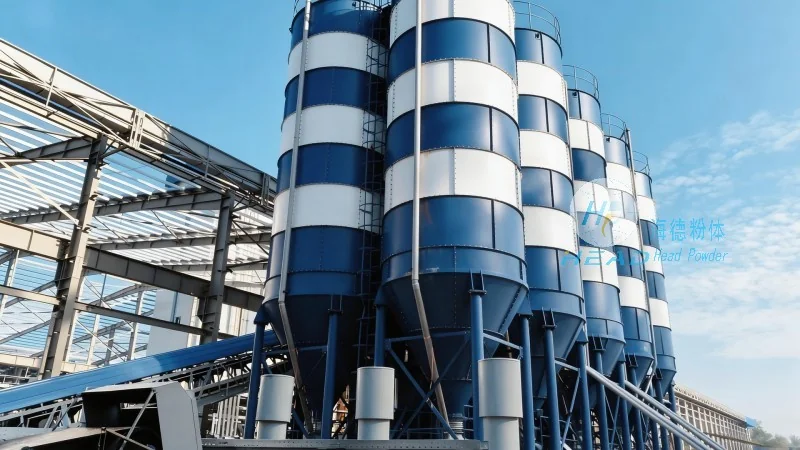
Barley malt, a key ingredient in brewing and other food applications, requires careful handling to preserve its quality and functionality. Conveying systems must ensure minimal product degradation, consistent flow, and compliance with hygiene standards. The primary methods used for transporting barley malt include gravity flow, mechanical conveyors, pneumatic systems, and automated robotic solutions. Each method has unique characteristics that make it suitable for different operational scenarios and production scales.
1. Gravity Flow Conveying Systems
Gravity flow systems utilize the natural force of gravity to move barley malt from one elevation to another. These systems typically consist of sloped chutes or troughs that allow the malt to slide down under the influence of gravity. The primary advantage of gravity flow is its simplicity and low energy consumption, as no external power is required for operation. This makes it an economical choice for short-distance transfers where the elevation difference is sufficient to drive the flow. However, the effectiveness of gravity flow is highly dependent on the angle of the chute and the moisture content of the malt. Excessive moisture can cause the malt to stick to the chute walls, leading to reduced flow rates and potential blockages. Additionally, gravity flow systems are limited by the vertical drop available and cannot handle long horizontal distances efficiently.
2. Mechanical Conveyors
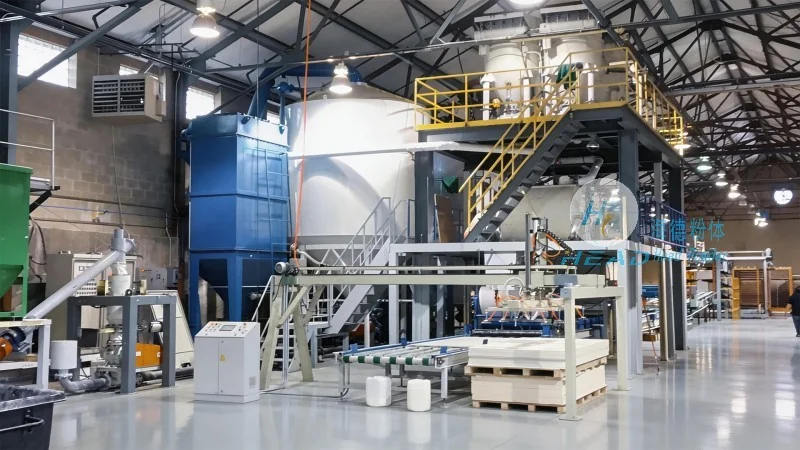
Mechanical conveyors, such as belt conveyors, screw conveyors, and chain conveyors, are widely used in malt processing due to their versatility and ability to handle various product types and quantities. Belt conveyors use a continuous belt to transport malt horizontally or at a slight incline, making them suitable for both short and medium-distance transfers. They offer high capacity and can be easily integrated with other processing equipment. Screw conveyors, or augers, are cylindrical screws that rotate to push malt forward. They are ideal for vertical or inclined transport and can handle dry or slightly moist malt. However, screw conveyors may cause more product degradation due to friction and compression, especially with delicate malt grains. Chain conveyors use a series of links or buckets to move malt, providing consistent and reliable transport. They are particularly effective for heavy or sticky materials but require more maintenance compared to other mechanical options.
3. Pneumatic Conveying Systems
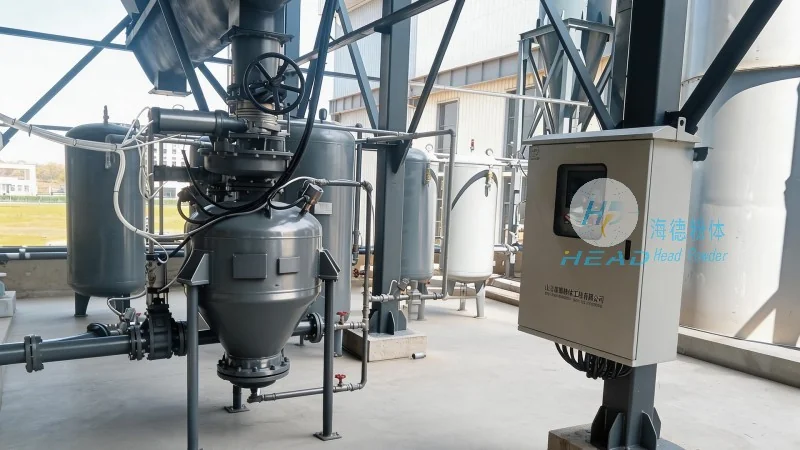
Pneumatic conveying systems use air or gas to transport barley malt through a network of pipes. These systems can be categorized into two main types: pressure and vacuum. Pressure systems force air through the pipe, pushing the malt forward, while vacuum systems create a negative pressure to draw the malt into the pipe. Pneumatic systems offer several advantages, including the ability to transport malt over long distances, even vertically, and to handle multiple points of loading and unloading. They also provide good product containment, reducing dust and contamination risks. However, pneumatic conveying can be energy-intensive, especially for long-distance or high-capacity applications. The system also requires careful design to prevent product degradation from high air velocities or excessive pressure drops. Additionally, the cost of equipment and maintenance for pneumatic systems is generally higher than for mechanical alternatives.
4. Automated Robotic and Conveyor Integration
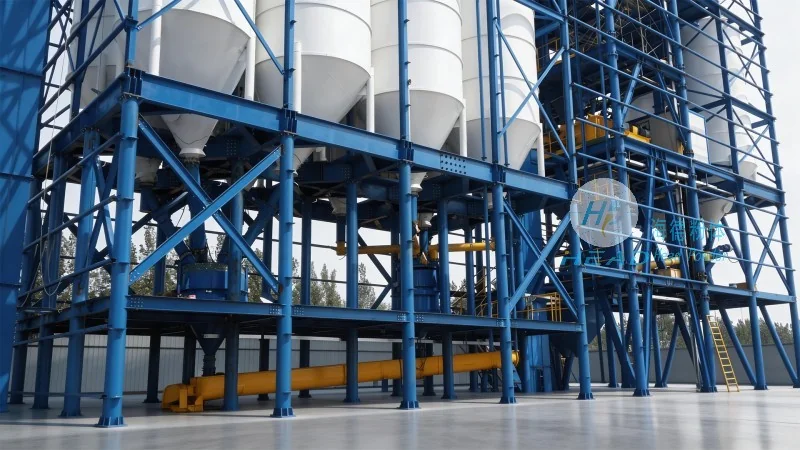
Advanced conveying solutions often involve the integration of robotic systems and automated controls to enhance efficiency and precision. These systems may include automated sorters, feeders, and conveyor networks that work in tandem to handle malt from receipt to processing. The use of sensors and real-time monitoring allows for dynamic adjustments to flow rates and product handling, ensuring optimal performance. Automated systems reduce labor costs and minimize human error, leading to improved consistency and quality control. However, the initial investment for such advanced solutions is substantial, and maintenance requirements can be more complex. They are typically employed in large-scale production facilities where the benefits of automation outweigh the costs.
Key Considerations for Selecting a Conveying Method
When choosing a barley malt conveying method, several factors must be considered to ensure the best fit for a specific application. The first consideration is the distance and elevation changes between the loading and unloading points. Gravity flow is suitable for short vertical drops, while mechanical or pneumatic systems are better for longer distances or complex layouts. The moisture content and bulk density of the malt also play a critical role. High moisture levels may require systems with better moisture control, such as enclosed conveyors or pneumatic systems with low air velocities. The production volume and throughput requirements are another key factor. High-volume operations may benefit from mechanical or pneumatic systems with higher capacity, while low-volume or batch processes might use gravity or smaller mechanical conveyors. Finally, the budget and maintenance capabilities of the facility must be evaluated. Simple gravity systems offer low maintenance costs, while advanced automated systems require skilled personnel and regular upkeep.
Conclusion
Each barley malt conveying method has its own set of advantages and disadvantages, and the optimal choice depends on the specific needs of the processing facility. Shandong HeadPowder Engineering Co., Ltd. offers expert consultation and customized solutions to help clients select and implement the most suitable conveying system. By carefully evaluating factors such as distance, product characteristics, and operational requirements, facilities can improve efficiency, reduce costs, and maintain the quality of their barley malt. Whether using gravity flow, mechanical conveyors, pneumatic systems, or automated solutions, the goal is to ensure reliable, hygienic, and cost-effective transportation of malt throughout the production process.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu