Với hơn 10 năm kinh nghiệm về vận chuyển khí nén, Headpowder Sơn Đông cung cấp hệ thống, thiết bị và quạt gió toàn chuỗi, đảm nhận các dự án kỹ thuật bột trọn gói trên toàn quốc.
Efficient mineral particle conveying is a critical aspect of industrial operations, ensuring smooth material handling from extraction to processing. The choice of conveying system depends on factors such as material type, volume, and operational environment. Understanding the available options helps businesses optimize their workflow and enhance productivity. This article explores various methods used for mineral particle transport, highlighting their applications and benefits.
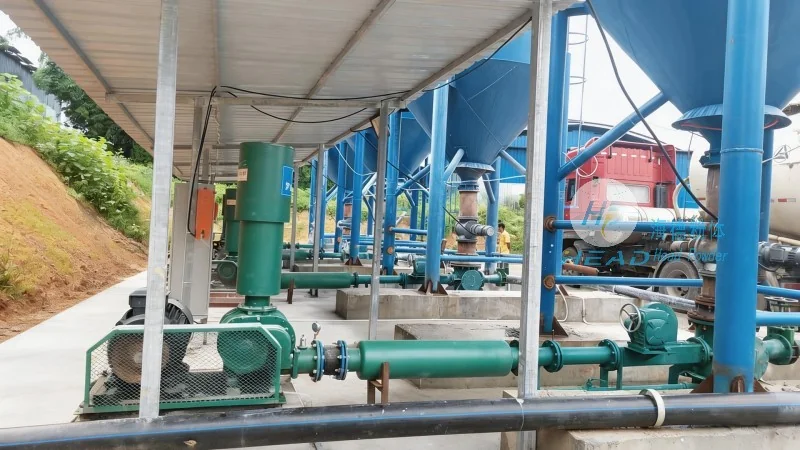
Common Conveying Systems for Mineral Particles
Screw conveyors, also known as auger conveyors, are widely used for transporting dry, free-flowing materials like minerals. These systems consist of a rotating screw within a tube, which moves material forward through a series of flights. Screw conveyors are particularly effective for vertical or inclined transport, making them suitable for elevating materials to higher levels or moving them over short distances. They are known for their simplicity, low maintenance, and ability to handle a wide range of particle sizes. The design can be customized to accommodate different material characteristics, ensuring efficient and reliable operation.
Advantages of Screw Conveyors in Mineral Processing
Screw conveyors offer several advantages for mineral particle transport. Their enclosed design minimizes dust and contamination, which is crucial for maintaining product quality and safety. They are also energy-efficient, as they require less power compared to other systems. Additionally, screw conveyors can operate in various environments, including dusty or wet conditions, without significant performance degradation. This makes them a preferred choice for industries dealing with abrasive or corrosive materials. The ability to adjust the screw speed allows for precise control over material flow, enabling businesses to match production rates with demand.
Belt Conveyors: Versatile and Durable Solutions
Belt conveyors are another popular option for mineral particle transport, especially in large-scale operations. These systems use a continuous belt looped over rollers to move materials horizontally or at a slight incline. Belt conveyors are highly efficient for transporting bulk materials over long distances, making them ideal for mining and processing facilities. They can handle a wide variety of materials, from fine powders to large rocks, and are capable of high throughput rates. The durability of the belt and rollers ensures long service life, reducing downtime and maintenance costs. Belt conveyors are also adaptable to different environments, including outdoor or harsh conditions, making them a reliable choice for industrial applications.
Key Features of Belt Conveyors for Mineral Handling
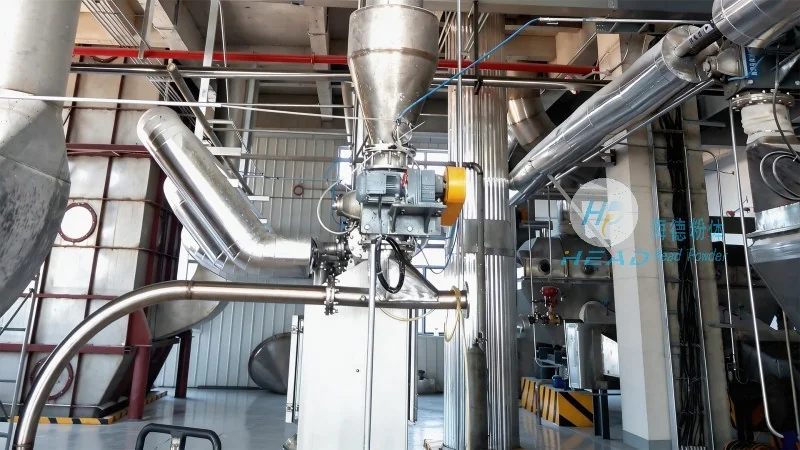
Belt conveyors offer several key features that enhance their performance in mineral processing. The use of heavy-duty belts and robust rollers provides excellent load-bearing capacity, allowing them to handle heavy loads without stretching or breaking. The modular design of belt conveyors enables easy installation and maintenance, with components that can be replaced individually. This reduces the overall cost of ownership and increases operational flexibility. Additionally, belt conveyors can be equipped with various accessories, such as idlers, pulleys, and tensioning systems, to optimize performance and extend service life. The ability to integrate with other equipment, like crushers or screens, makes belt conveyors a central part of many material handling systems.
Pneumatic Conveying Systems: Ideal for Dusty or Hazardous Materials
Pneumatic conveying systems use air or other gases to transport mineral particles through a pipeline. These systems are particularly suitable for materials that are dusty, abrasive, or hazardous, as they eliminate the need for direct contact with the material. Pneumatic conveyors can be categorized into pressure and vacuum types, each with its own advantages. Pressure systems are used for short to medium distances and high material loads, while vacuum systems are ideal for long distances and low loads. Pneumatic conveying offers high efficiency and flexibility, as it can transport materials through complex layouts and multiple points. The enclosed system also prevents dust emissions, improving workplace safety and environmental compliance.
Benefits of Pneumatic Conveying for Mineral Particle Transport
Pneumatic conveying systems provide several benefits for mineral particle transport. They are highly effective in handling fine powders and granules, which are difficult to transport using other methods. The ability to transport materials in a closed system reduces dust and contamination, making them suitable for food, pharmaceutical, and chemical industries. Pneumatic conveyors also offer high throughput rates and can be integrated with other processing equipment, such as mixers or classifiers. The flexibility of the system allows for easy expansion or modification, adapting to changing production needs. Additionally, pneumatic conveying reduces the risk of material spillage and damage, ensuring product integrity throughout the transport process.
Hydraulic Conveying: High-Pressure Applications
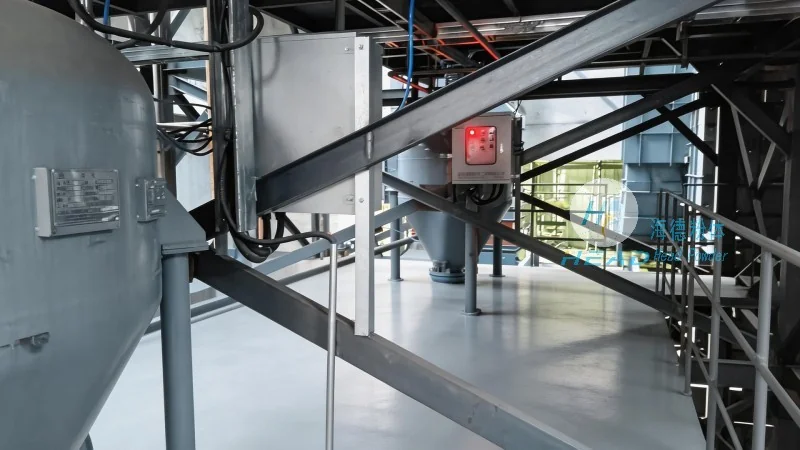
Hydraulic conveying systems use high-pressure water or other fluids to transport mineral particles, typically in mining and heavy industry applications. These systems are designed for high-volume, high-pressure transport, making them suitable for moving large quantities of materials over long distances. Hydraulic conveyors are particularly effective for abrasive materials, as the fluid helps to reduce wear and tear on the system components. The enclosed pipeline system prevents dust and contamination, ensuring a clean and safe operation. Hydraulic conveying offers high efficiency and reliability, with minimal maintenance requirements. However, these systems require significant infrastructure and energy input, making them suitable for large-scale operations.
Applications and Advantages of Hydraulic Conveying
Hydraulic conveying is commonly used in mining operations for transporting ore from the mine to processing facilities. The high-pressure fluid provides the necessary force to move materials through the pipeline, even over steep inclines or long distances. The system is capable of handling large volumes of material, making it ideal for high-production mines. The enclosed design minimizes environmental impact and ensures compliance with regulations. Hydraulic conveyors also offer the advantage of being able to transport materials with high moisture content, which is beneficial for certain mining processes. The ability to adjust the fluid pressure allows for precise control over material flow, ensuring consistent performance.
Customized Solutions from Shandong HeadPowder Engineering Co., Ltd.
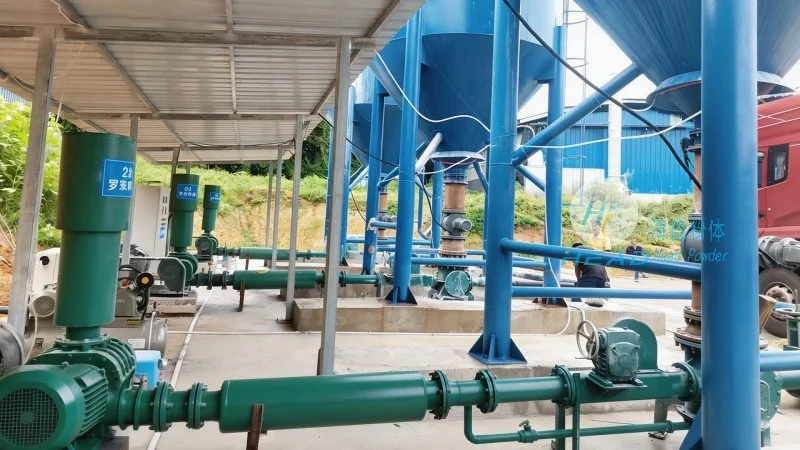
Shandong HeadPowder Engineering Co., Ltd., a leading provider of mineral processing solutions, offers customized conveying systems tailored to the specific needs of industrial clients. With years of experience in the industry, HeadPowder specializes in designing and manufacturing efficient mineral particle conveying equipment. The company's team of engineers works closely with clients to understand their operational requirements and develop solutions that optimize material handling and productivity. HeadPowder's products are known for their durability, reliability, and adaptability, ensuring long-term performance and minimal maintenance. The company provides comprehensive support, including installation, maintenance, and technical assistance, to ensure clients achieve the best results from their conveying systems.
Key Features of HeadPowder's Conveying Solutions
HeadPowder Engineering's conveying systems are designed with a focus on efficiency, durability, and customization. The company uses high-quality materials and advanced manufacturing techniques to ensure that its products meet the highest standards of performance and reliability. The systems are available in various configurations, including screw, belt, pneumatic, and hydraulic, allowing clients to choose the most suitable option for their specific application. HeadPowder also offers integrated solutions, combining different types of conveyors to create a complete material handling system. This approach ensures seamless operation and optimal performance across the entire production process. The company's commitment to innovation and customer satisfaction has made it a trusted partner for businesses in the mineral processing industry.
Conclusion: Choosing the Right Conveying System
Selecting the appropriate mineral particle conveying system is crucial for optimizing industrial operations and enhancing productivity. The choice depends on factors such as material characteristics, operational requirements, and environmental considerations. Each conveying method has its own advantages and limitations, making it essential to evaluate the specific needs of the application. By understanding the options available and consulting with experts like Shandong HeadPowder Engineering Co., Ltd., businesses can make informed decisions that lead to efficient, reliable, and cost-effective material handling solutions. Whether using screw, belt, pneumatic, or hydraulic systems, the right choice can significantly improve workflow, reduce downtime, and ensure the long-term success of industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu