Với hơn 10 năm kinh nghiệm về vận chuyển khí nén, Headpowder Sơn Đông cung cấp hệ thống, thiết bị và quạt gió toàn chuỗi, đảm nhận các dự án kỹ thuật bột trọn gói trên toàn quốc.
For the efficient transportation of barley malt in industrial settings, various methods are employed to ensure smooth and reliable material handling. The choice of method depends on factors such as the volume of malt, the distance to be covered, and the specific requirements of the production process. This article explores the common approaches used for barley malt transportation, highlighting the capabilities and benefits of each method.
Company Introduction
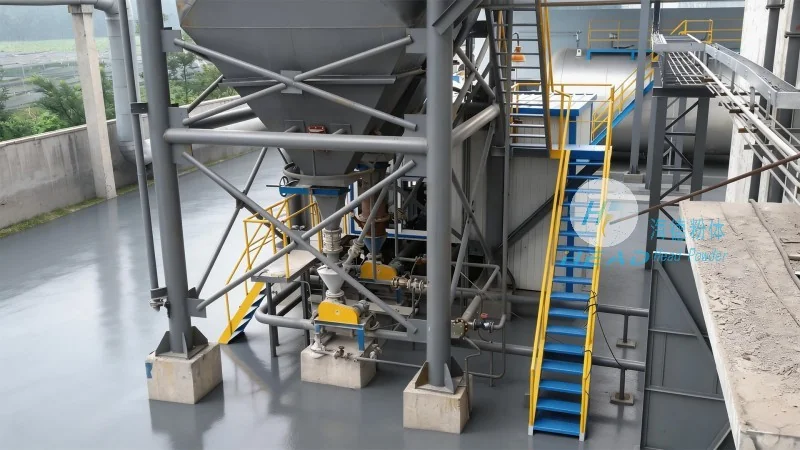
HeadPowder, a leading provider in the field, is dedicated to delivering high-quality solutions for malt handling. As Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, the company specializes in engineering and manufacturing equipment tailored to the needs of the brewing and food processing industries. With years of experience, HeadPowder offers reliable and efficient transportation systems that enhance productivity and maintain the quality of barley malt throughout the process.
Common Methods for Barley Malt Transportation
Several methods are widely used for transporting barley malt from storage to processing areas. The most common approaches include belt conveyors, bucket elevators, and pneumatic conveyors. Each method has its own advantages and is suitable for different operational conditions.
Belt Conveyors
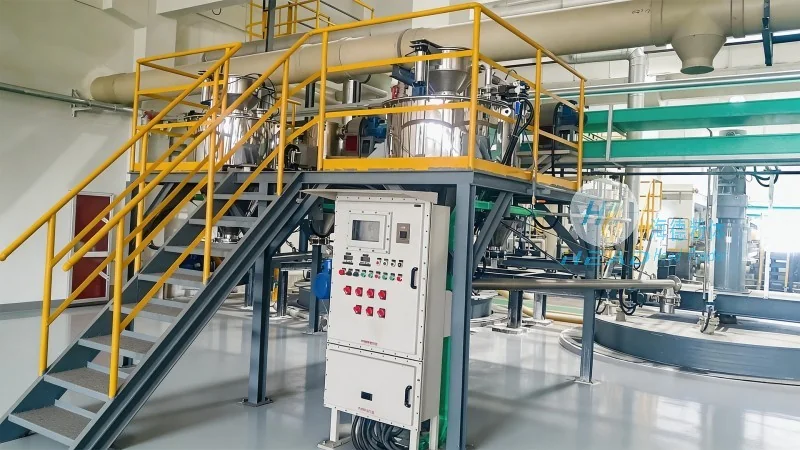
Belt conveyors are among the most prevalent systems for barley malt transportation. These systems utilize a continuous belt, typically made of durable materials like rubber or PVC, to move malt from one location to another. The belt is supported by rollers and can be configured in various configurations, including horizontal, inclined, or even vertical sections. This flexibility allows for the transportation of malt over long distances with minimal maintenance. Belt conveyors are particularly effective for moving large volumes of malt at a steady pace, making them ideal for bulk handling in breweries and malting facilities.
Bucket Elevators
Bucket elevators are another essential method for vertical or inclined transportation of barley malt. These systems consist of a vertical or inclined frame with a series of buckets attached to a chain or belt. As the buckets move up or down, they carry the malt from the lower to the upper level. Bucket elevators are known for their high capacity and ability to handle a wide range of materials, including barley malt. They are often used to transport malt from storage silos to the top of processing equipment, ensuring a consistent and efficient flow of material. The enclosed design of bucket elevators also helps in maintaining the quality of the malt by preventing contamination and dust dispersion.
Pneumatic Conveyors
Pneumatic conveyors use air pressure to transport barley malt through a system of pipes. This method is particularly suitable for transporting malt over short to medium distances and for handling fine or powdery malt products. The malt is carried by air currents within the pipes, which can be arranged in a straight or curved path. Pneumatic conveyors offer the advantage of being able to transport malt in a closed system, reducing dust and ensuring a clean environment. However, they may require more energy compared to other methods and are generally more suitable for smaller volumes or specific applications where dust control is critical.
Advantages of Modern Transportation Systems
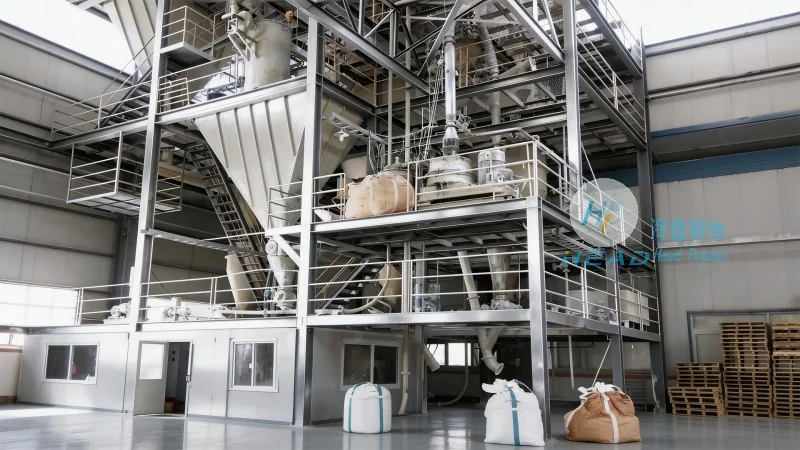
Modern transportation systems for barley malt, such as those offered by HeadPowder, provide several key advantages. These systems are designed to enhance efficiency, reduce labor costs, and maintain the quality of the malt. By automating the transportation process, companies can achieve consistent and reliable material flow, minimizing downtime and improving overall productivity. Additionally, advanced materials and engineering ensure that the equipment can withstand the abrasive nature of barley malt, reducing wear and tear and extending the lifespan of the machinery.
Application in Brewing and Food Processing
Barley malt transportation plays a crucial role in the brewing and food processing industries. In breweries, efficient transportation ensures that malt is delivered to the mashing tanks in optimal condition, which is essential for producing high-quality beer. The systems must be able to handle the varying moisture content and size of malt grains without causing damage or degradation. Similarly, in food processing facilities, the transportation of malt is vital for producing malt-based products like malt extract or malt syrup. The reliability of the transportation system directly impacts the final product quality and consistency.
Customized Solutions from HeadPowder
HeadPowder understands that each facility has unique requirements for barley malt transportation. Therefore, the company offers customized solutions tailored to the specific needs of its clients. By working closely with customers, HeadPowder engineers can design and manufacture transportation systems that meet exact specifications, including the required capacity, distance, and operational conditions. The company’s expertise in engineering and manufacturing ensures that the solutions are not only efficient but also durable and cost-effective. With a focus on quality and customer satisfaction, HeadPowder provides comprehensive support, from initial consultation to installation and maintenance, ensuring that the transportation systems operate at peak performance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu