Với hơn 10 năm kinh nghiệm về vận chuyển khí nén, Headpowder Sơn Đông cung cấp hệ thống, thiết bị và quạt gió toàn chuỗi, đảm nhận các dự án kỹ thuật bột trọn gói trên toàn quốc.
For industries dealing with magnesium sulfate, selecting the right material handling system is crucial for operational efficiency and environmental compliance. Pneumatic conveying, particularly for magnesium sulfate, offers a modern solution that combines high performance with sustainable practices. This article explores the benefits of pneumatic conveying systems for magnesium sulfate, highlighting how they enhance process reliability while minimizing environmental impact.
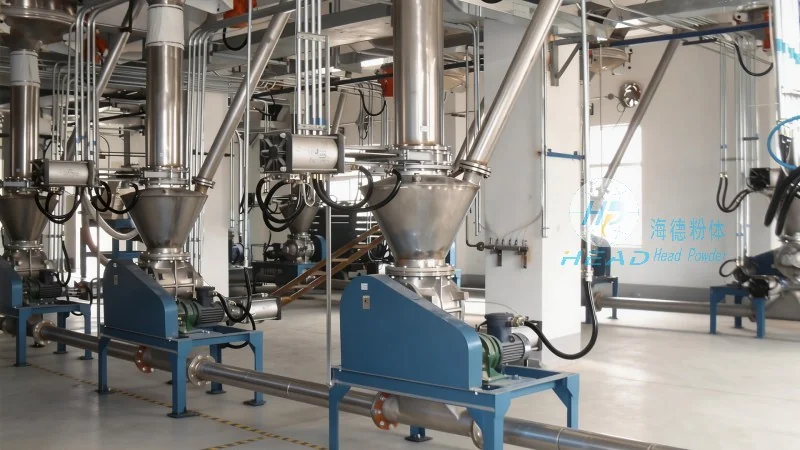
Understanding Pneumatic Conveying Technology
Pneumatic conveying systems use air or other gases to transport bulk materials like magnesium sulfate through a pipeline network. Unlike traditional methods such as belt conveyors or bucket elevators, pneumatic systems provide a closed-loop operation that reduces dust emissions and improves safety. The technology operates by creating a pressure differential, either through positive pressure (blowing air into the system) or negative pressure (sucking material into the system), to move the material from the source to the destination. This method is especially effective for handling fine powders and granules, which are common in magnesium sulfate applications.
Key Advantages of Magnesium Sulfate Pneumatic Conveying
Implementing a pneumatic conveying system for magnesium sulfate offers several significant advantages. First, it enhances operational efficiency by reducing downtime and labor costs associated with manual handling or traditional bulk transport. The automated process ensures consistent material flow, which is critical for maintaining production rates in manufacturing facilities. Second, environmental benefits are substantial. By containing the material within a sealed system, pneumatic conveying minimizes dust dispersion into the environment, aligning with regulatory standards for air quality. This not only reduces the risk of contamination but also lowers the need for additional dust control measures, such as baghouses or scrubbers, which can be costly to maintain.
Customized Solutions from HeadPowder
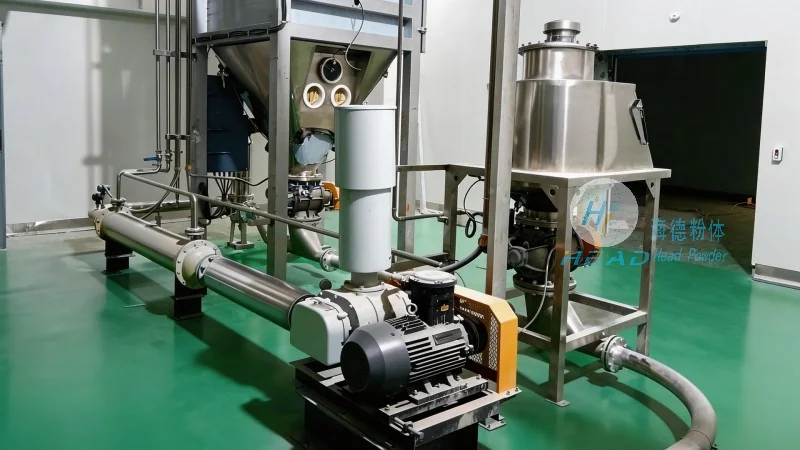
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the specific needs of magnesium sulfate applications. With decades of experience in the industry, HeadPowder understands the unique challenges of handling magnesium sulfate, including its hygroscopic nature and potential for dust generation. The company’s team of engineers works closely with clients to assess their operational requirements, process flow, and environmental constraints to develop customized solutions that maximize efficiency and sustainability.
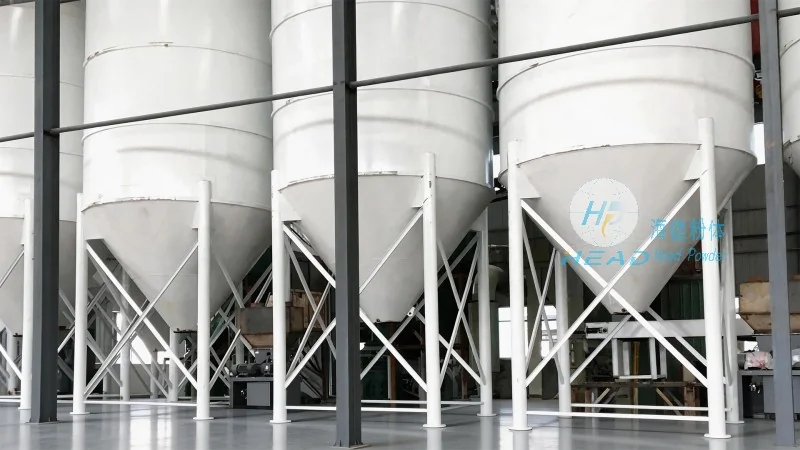
System Components and Design Considerations
A typical magnesium sulfate pneumatic conveying system consists of several key components, each designed to optimize performance and reliability. These include the material feed hopper, which ensures a consistent flow of material into the system; the conveyor line, which transports the material through the pipeline; and the discharge equipment, which delivers the material to the final destination. The system also incorporates air handling units, such as blowers or vacuum pumps, to generate the necessary pressure or suction. HeadPowder’s engineers pay close attention to material properties, such as particle size distribution and moisture content, when designing the system to ensure optimal performance and prevent issues like blockages or corrosion.
Operational Efficiency and Cost Savings
One of the primary benefits of pneumatic conveying for magnesium sulfate is the reduction in operational costs. By eliminating the need for multiple handling steps and reducing equipment wear and tear, companies can achieve significant savings over time. The automated nature of the system also minimizes labor requirements, allowing personnel to focus on other critical tasks. Additionally, the closed-loop design reduces energy consumption compared to open systems, further contributing to cost savings and environmental sustainability.
Environmental Compliance and Safety
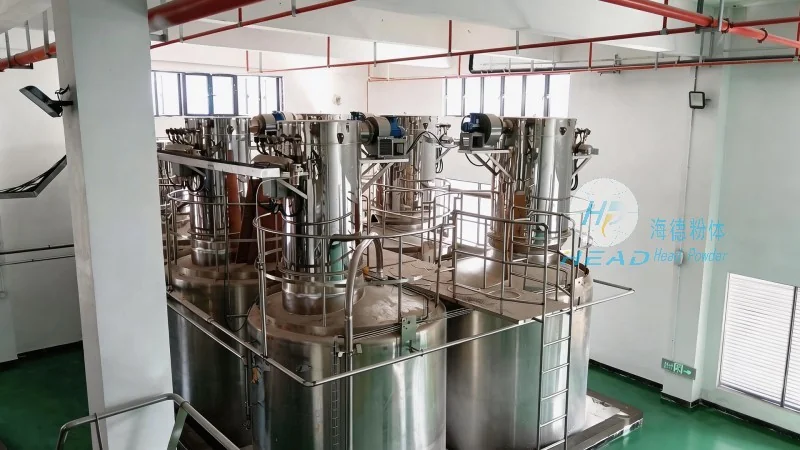
With increasing emphasis on environmental regulations, the environmental benefits of pneumatic conveying are more important than ever. The sealed system prevents dust from escaping into the workplace or the surrounding environment, reducing the risk of respiratory issues for workers and minimizing the impact on local ecosystems. HeadPowder’s systems are designed to meet or exceed industry standards for air quality and safety, ensuring that clients can operate with confidence while complying with regulatory requirements.
Conclusion and Future Outlook
Pneumatic conveying represents a forward-thinking approach to handling magnesium sulfate, offering a balance of efficiency, sustainability, and reliability. By leveraging advanced technology and customized solutions, companies can enhance their operational performance while reducing their environmental footprint. Shandong HeadPowder Engineering Co., Ltd. remains committed to providing innovative material handling solutions that meet the evolving needs of the industry, helping clients achieve their goals for productivity and sustainability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu