Với hơn 10 năm kinh nghiệm về vận chuyển khí nén, Headpowder Sơn Đông cung cấp hệ thống, thiết bị và quạt gió toàn chuỗi, đảm nhận các dự án kỹ thuật bột trọn gói trên toàn quốc.
HeadPowder, a leading provider in material handling solutions, specializes in advanced pneumatic conveying systems tailored for activated carbon powder. This article explores the benefits and applications of pneumatic conveying for this specific material, highlighting how it addresses the challenges of transporting fine powders while ensuring operational efficiency and environmental sustainability.
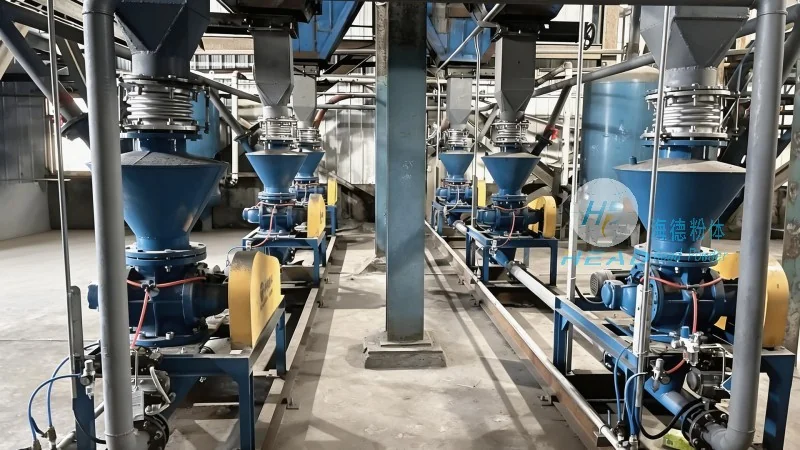
Introduction to Pneumatic Conveying for Activated Carbon Powder
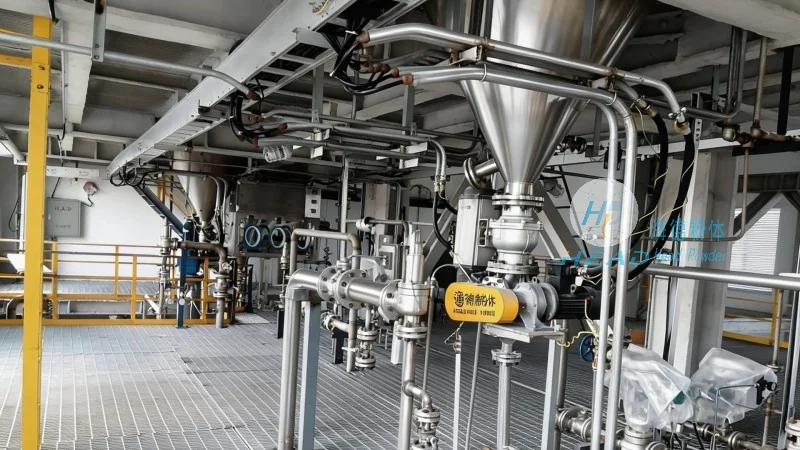
Activated carbon powder is widely used in various industries, including water treatment, air purification, and chemical processing. Its fine particle size and high dust generation potential make traditional handling methods, such as manual handling or mechanical conveying, inefficient and often hazardous. Pneumatic conveying offers a superior alternative by utilizing air to transport the powder, eliminating the need for mechanical components that can cause contamination or damage to the material.
Efficiency and Environmental Advantages of Pneumatic Conveying
One of the primary benefits of pneumatic conveying for activated carbon powder is its high efficiency in material transport. The system can handle large volumes of powder with minimal downtime, reducing operational costs and increasing productivity. Additionally, this method is highly eco-friendly as it eliminates the need for water or other liquids in the conveying process, preventing water pollution and reducing the carbon footprint associated with traditional handling techniques.
Technical Features and System Components
The pneumatic conveying system for activated carbon powder typically includes several key components: a hopper for material storage, a blower or compressor to generate airflow, a pipeline network to transport the powder, and a receiver for the material's final destination. The system can be designed as a dilute-phase or dense-phase conveyor, depending on the specific requirements of the application. Dilute-phase systems are suitable for long-distance transport and high-volume applications, while dense-phase systems are ideal for short-distance transport and sensitive materials that require minimal particle breakage.
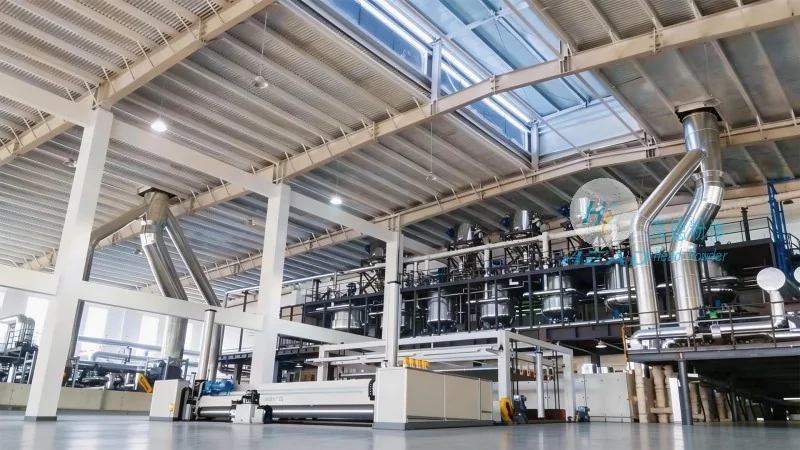
Application Scenarios and Industry Impact
HeadPowder's pneumatic conveying solutions are applied in diverse industries where activated carbon powder is a critical component. In the water treatment industry, the system efficiently transports activated carbon to filtration systems, ensuring optimal water purification. In the chemical industry, it facilitates the handling of activated carbon in production lines, enhancing process efficiency. The system's ability to maintain the purity and quality of the activated carbon powder is crucial, as any contamination can affect the performance of downstream processes.
Conclusion and Company Overview
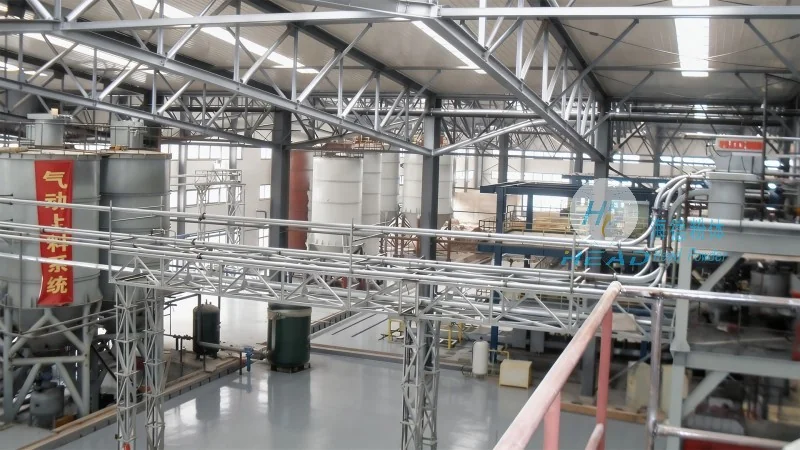
HeadPowder Engineering Co., Ltd., based in Shandong, China, is committed to providing innovative and sustainable material handling solutions. Our pneumatic conveying systems for activated carbon powder are designed to meet the highest standards of efficiency, environmental responsibility, and operational reliability. By leveraging advanced technology and expert engineering, we help industries achieve their material handling goals while minimizing environmental impact. Contact HeadPowder for more information on how our solutions can enhance your operational efficiency and contribute to a greener future.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu