Với hơn 10 năm kinh nghiệm về vận chuyển khí nén, Headpowder Sơn Đông cung cấp hệ thống, thiết bị và quạt gió toàn chuỗi, đảm nhận các dự án kỹ thuật bột trọn gói trên toàn quốc.
HeadPowder, a leading provider of advanced material handling systems, specializes in dry coffee pneumatic conveying technology. This innovative solution represents a significant advancement in the efficient and eco-friendly transportation of coffee beans and other dry bulk materials. By leveraging air pressure to move materials, the system offers a seamless, low-maintenance approach to handling delicate and valuable products like coffee. The company is headquartered in Shandong, China, with a strong commitment to delivering high-quality, sustainable solutions for the coffee industry.
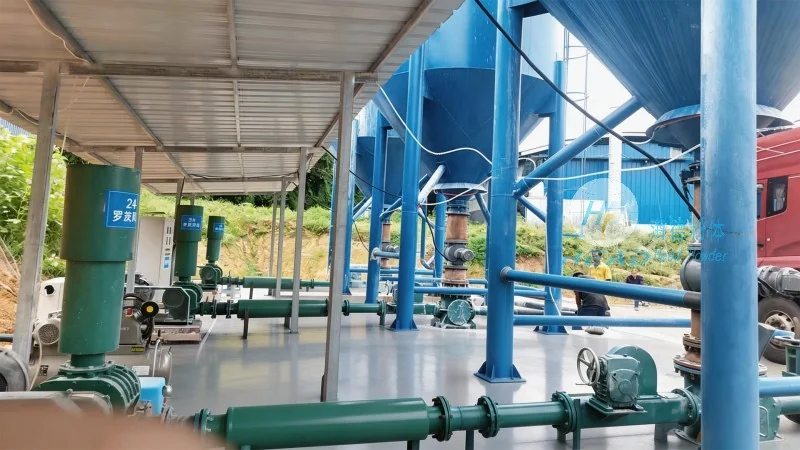
Understanding Dry Coffee Pneumatic Conveying
At the core of this technology is the use of air as the primary medium to transport dry coffee beans or other similar materials. Unlike traditional methods such as belt conveyors or bucket elevators, pneumatic conveying systems eliminate the need for physical contact between the material and the conveying equipment. This is particularly advantageous for coffee, as it prevents damage to the beans' surface and preserves their quality, aroma, and flavor profile. The system operates by creating a pressure differential, either through vacuum or pressure, to draw or push the material through a network of pipes. This method ensures that the coffee remains intact, maintaining its premium characteristics throughout the handling process.
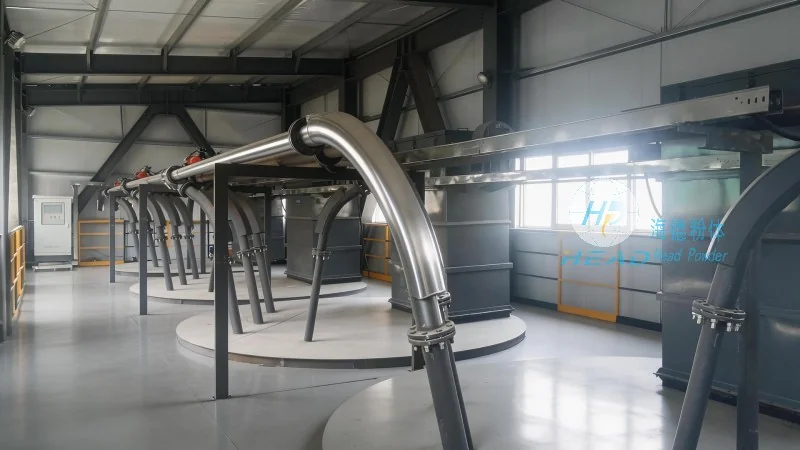
Key Advantages of Dry Coffee Pneumatic Conveying
One of the most notable benefits of this technology is its efficiency. The system can handle large volumes of coffee beans with minimal energy consumption compared to traditional mechanical systems. This not only reduces operational costs but also contributes to a lower carbon footprint, aligning with modern sustainability goals. Additionally, the lack of moving parts in the conveying line reduces maintenance requirements, leading to lower downtime and increased productivity. The system's flexibility allows for easy integration into existing production lines, making it a cost-effective upgrade for coffee processing facilities. Furthermore, the enclosed nature of the system prevents dust and contamination, ensuring that the final product meets stringent quality and safety standards. This is crucial for coffee producers who must adhere to high hygiene and regulatory requirements.
Environmental Impact and Sustainability
Environmental considerations are a critical factor in modern industrial operations, and dry coffee pneumatic conveying excels in this area. By eliminating the need for water or other cleaning agents in the conveying process, the system reduces water usage and waste generation. The use of compressed air, when sourced from energy-efficient compressors, further minimizes the environmental impact. The reduced need for physical handling equipment also lowers the risk of accidents and injuries, contributing to a safer working environment. Moreover, the system's low energy consumption and minimal waste make it an attractive option for companies committed to reducing their environmental footprint. This aligns with global trends towards sustainable manufacturing practices, making it a preferred choice for environmentally conscious coffee producers.
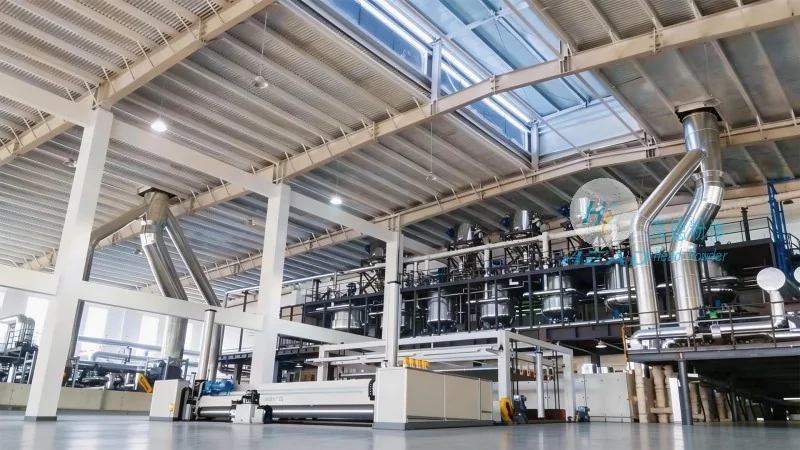
Application in Coffee Processing
Dry coffee pneumatic conveying is widely used in various stages of coffee processing, from raw bean handling to packaging. In the initial stages, the system efficiently transports freshly harvested coffee beans from storage silos or drying areas to processing facilities. This ensures that the beans are handled gently, preserving their natural oils and flavor compounds. During the roasting process, the system can convey roasted beans to packaging lines without exposing them to external contaminants. The enclosed system also helps maintain consistent temperature and humidity levels, which are vital for preserving the coffee's aroma and taste. For decaffeinated coffee production, the system can handle solvents and other processing agents safely and efficiently, ensuring that the final product is free from residues. The versatility of the technology makes it suitable for both small-scale artisanal coffee roasters and large-scale commercial operations, providing a scalable solution for different production capacities.
Customization and Integration
HeadPowder understands that each coffee processing facility has unique requirements. Therefore, the company offers customized pneumatic conveying systems tailored to specific needs. This includes the design of specialized components such as cyclone separators, filters, and material feeders to ensure optimal performance. The systems can be integrated with existing equipment, such as roasters, grinders, and packaging machines, without disrupting current operations. HeadPowder's engineering team works closely with clients to assess their production processes, identify bottlenecks, and develop solutions that enhance efficiency and reduce costs. The company's commitment to quality and innovation ensures that each system is built to meet the highest standards, providing long-term reliability and performance. Whether it's a new installation or an upgrade to an existing system, HeadPowder's solutions are designed to deliver maximum value and efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu