Với hơn 10 năm kinh nghiệm về vận chuyển khí nén, Headpowder Sơn Đông cung cấp hệ thống, thiết bị và quạt gió toàn chuỗi, đảm nhận các dự án kỹ thuật bột trọn gói trên toàn quốc.
Phosphate rock powder is a critical raw material in the production of fertilizers and other industrial chemicals. The efficient and safe transportation of this fine powder is essential for maintaining production efficiency and minimizing environmental impact. Pneumatic conveying systems offer a superior solution for handling phosphate rock powder, combining high efficiency with environmental sustainability. This article explores the benefits, technical aspects, and practical applications of pneumatic conveying for phosphate rock powder, highlighting how companies like Shandong HeadPowder Engineering Co., Ltd. (HeadPowder) provide advanced solutions tailored to industry needs.
About HeadPowder: Your Partner in Advanced Material Handling
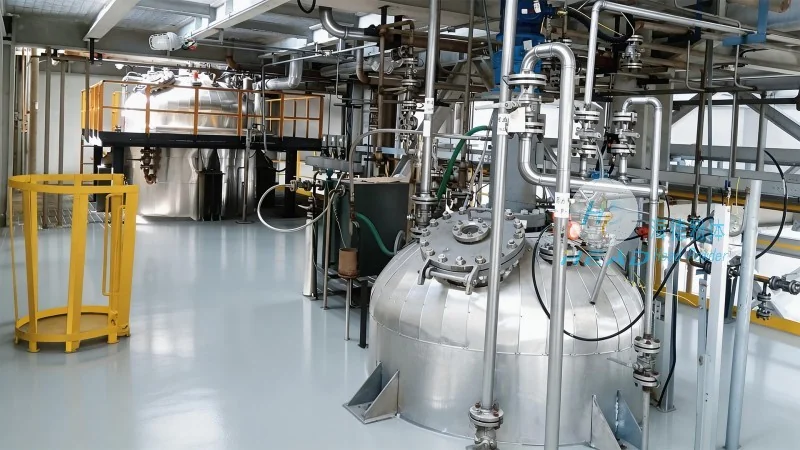
HeadPowder, a leading provider of material handling solutions, specializes in the design, manufacturing, and implementation of pneumatic conveying systems. With a focus on innovation and customer satisfaction, HeadPowder serves industries that rely on the reliable transport of fine powders. The company is headquartered in Shandong, China, and has established a reputation for delivering high-quality, efficient, and environmentally conscious systems. By leveraging years of experience and technical expertise, HeadPowder ensures that its solutions meet the stringent requirements of modern industrial operations, particularly in the fertilizer and chemical sectors where phosphate rock powder is a key component.
Key Advantages of Pneumatic Conveying for Phosphate Rock Powder
Traditional methods of transporting phosphate rock powder, such as belt conveyors or bucket elevators, often face challenges related to dust generation, material degradation, and operational inefficiencies. Pneumatic conveying addresses these issues through its unique design and operation. The primary advantages of using a pneumatic system for phosphate rock powder include:
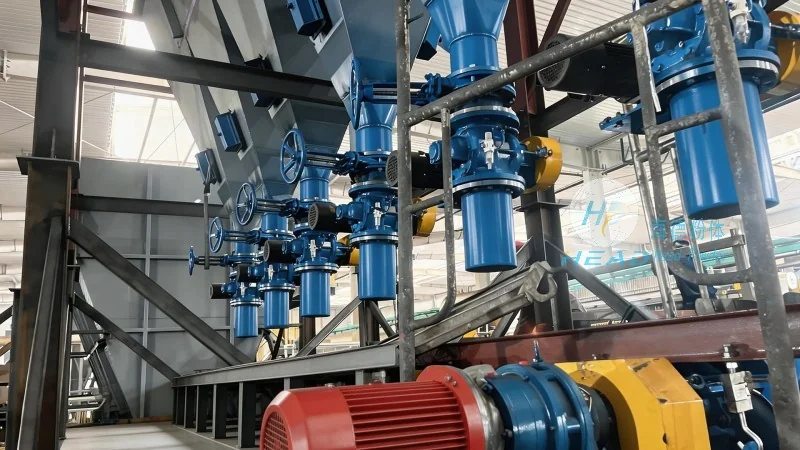
Efficiency and Speed: Pneumatic conveying allows for rapid and continuous transport of phosphate rock powder over long distances with minimal downtime. The system can handle high flow rates, ensuring that production lines operate at optimal capacity.
Environmental Protection: Unlike mechanical systems that may generate significant dust and noise, pneumatic conveying systems are enclosed, reducing emissions and noise pollution. This makes them compliant with environmental regulations and safer for both personnel and the environment.
Material Integrity: The enclosed nature of the system prevents contamination from external sources and minimizes the risk of material degradation due to exposure to air or moisture. This is crucial for maintaining the quality of phosphate rock powder, which is sensitive to changes in moisture and temperature.
Flexibility and Scalability: Pneumatic conveying systems can be easily customized to fit various production scales and layouts. They can be integrated with existing facilities or designed as standalone solutions, providing flexibility in system expansion or modification.
Technical Aspects of Pneumatic Conveying Systems
The effectiveness of a pneumatic conveying system for phosphate rock powder depends on several technical factors. These include the type of system (positive pressure, negative pressure, or a combination), the design of the conveying line, and the selection of appropriate components. HeadPowder’s engineers carefully evaluate the specific requirements of each project to determine the optimal system configuration.
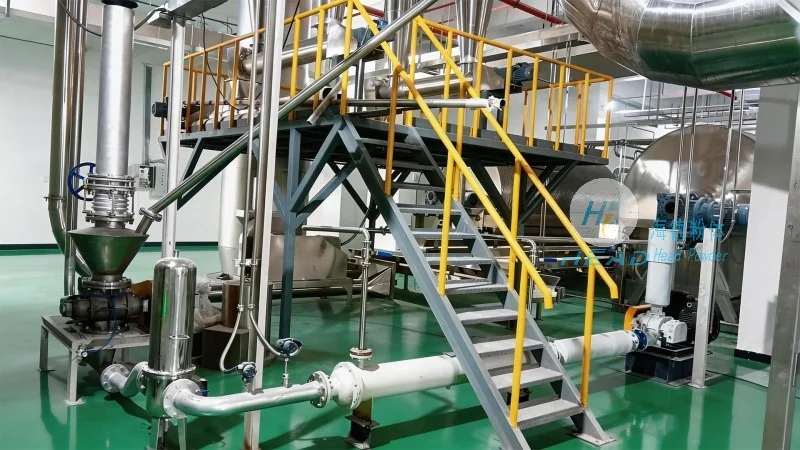
For phosphate rock powder, positive pressure systems are commonly used due to their ability to handle fine powders and provide consistent flow. These systems use a blower or compressor to generate air pressure that propels the powder through the pipeline. The design of the pipeline, including the diameter, length, and number of bends, is critical to maintaining the flow rate and preventing blockages. HeadPowder employs advanced computational fluid dynamics (CFD) and engineering principles to model the system and ensure smooth operation.
Key components of a pneumatic conveying system for phosphate rock powder include the hopper, feeder, blower, pipeline, and receiver. The hopper is designed to store the phosphate rock powder and provide a consistent feed to the feeder. The feeder controls the flow rate of the powder into the system, ensuring stable operation. The blower generates the necessary air pressure to move the powder. The pipeline transports the powder and air mixture, and the receiver collects the material at the destination. HeadPowder’s systems are equipped with high-quality components from reputable manufacturers, ensuring durability and reliability.
Application Scenarios and Industry Impact
Pneumatic conveying systems are widely used in the fertilizer industry for transporting phosphate rock powder from storage to processing units, and from processing to packaging. They are also applicable in other industries where fine powders are involved, such as chemical manufacturing and food processing. The use of pneumatic conveying in these industries has led to significant improvements in operational efficiency and environmental performance.
In the fertilizer industry, for example, pneumatic conveying allows for the seamless integration of phosphate rock powder with other raw materials, such as nitrogen and potassium, ensuring a consistent blend for the final product. This not only improves production throughput but also reduces waste and energy consumption. The environmental benefits are particularly notable, as the enclosed system minimizes dust emissions, which are a major concern in industrial operations.
HeadPowder’s pneumatic conveying solutions have been successfully implemented in various projects across China and other regions. The company’s expertise in system design and integration has enabled clients to achieve higher productivity, lower operational costs, and better compliance with environmental regulations. By partnering with HeadPowder, businesses can enhance their material handling capabilities and stay competitive in the market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu