Với hơn 10 năm kinh nghiệm về vận chuyển khí nén, Headpowder Sơn Đông cung cấp hệ thống, thiết bị và quạt gió toàn chuỗi, đảm nhận các dự án kỹ thuật bột trọn gói trên toàn quốc.
Malted barley is a crucial ingredient in the brewing industry, and efficient conveying methods are essential for maintaining quality and operational efficiency. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in delivering tailored solutions for malted barley handling and transportation. This article explores the various methods used to convey malted barley, highlighting the key considerations and technologies employed in modern processing facilities.
Gravity Conveying Systems
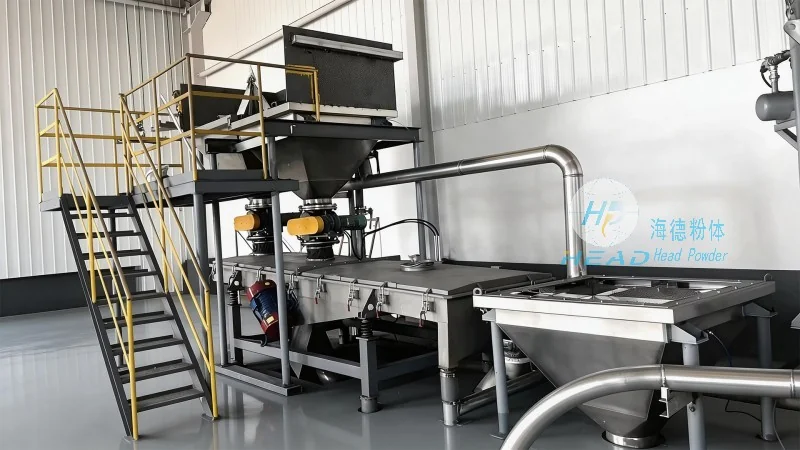
Gravity conveying relies on the natural force of gravity to move malted barley from one point to another. This method is often used for short distances and when the material has a relatively uniform size and shape. HeadPowder Engineering offers gravity chutes and sloped conveyors that are designed to minimize friction and prevent product damage. These systems are particularly effective for transferring malted barley from storage silos to processing areas, ensuring a smooth and continuous flow without the need for additional power.
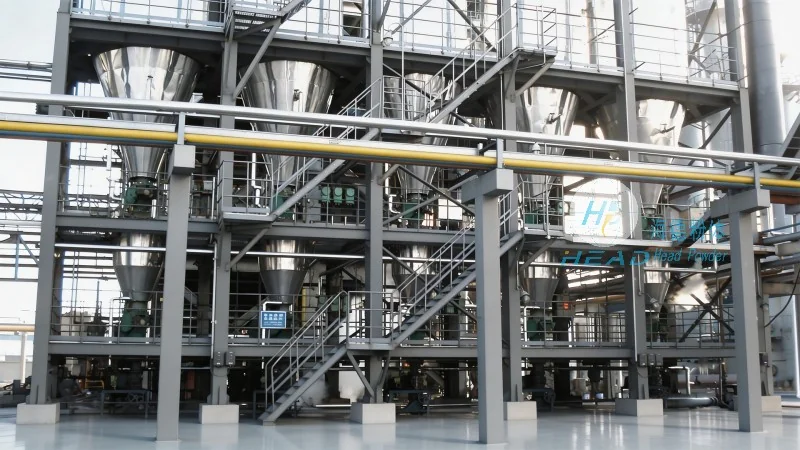
Mechanical Conveying Solutions
Mechanical conveying systems utilize mechanical components to move malted barley, offering greater control and adaptability compared to gravity systems. Two common types include belt conveyors and screw conveyors. Belt conveyors use a continuous belt to transport malted barley over a series of rollers, making them suitable for both horizontal and inclined applications. HeadPowder Engineering’s belt conveyor systems are engineered with durable materials and adjustable speed controls, ensuring reliable performance in high-volume malted barley handling operations. Screw conveyors, also known as augers, use a rotating screw to push malted barley through a tube. These systems are ideal for vertical or inclined transport and are often used in combination with other equipment to create a complete malted barley processing line.
Air Conveying (Pneumatic Conveying)
Air conveying, or pneumatic conveying, uses compressed air to transport malted barley in a closed system. This method is highly efficient for long-distance and high-volume transport, as it can move material over significant distances with minimal labor. HeadPowder Engineering provides both positive and negative pressure air conveying systems. Positive pressure systems blow air through the conveying line, while negative pressure systems create a vacuum to draw material in. The choice between these systems depends on the specific application, such as the distance to be covered and the need to prevent dust emissions. Air conveying is particularly advantageous for handling malted barley in environments where dust control is critical, as the enclosed system prevents contamination and maintains product quality.
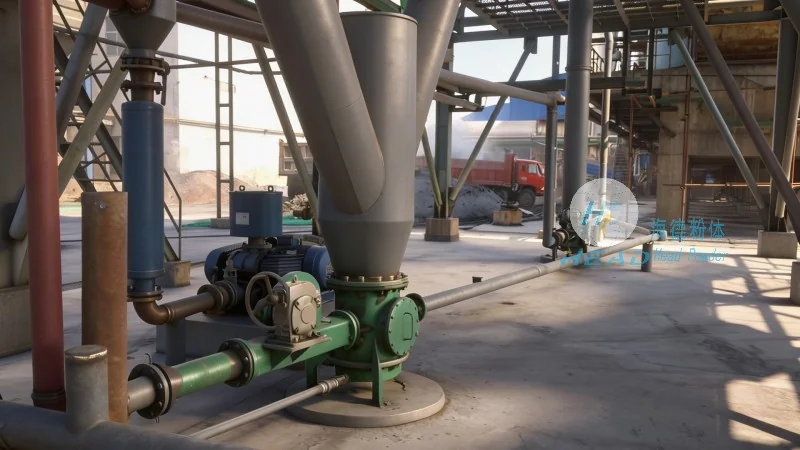
Key Considerations for Malted Barley Conveying
When selecting a conveying method for malted barley, several factors must be considered to ensure optimal performance and product integrity. First, the physical properties of the malted barley, such as its moisture content, size, and density, play a significant role. For example, wetter or more delicate malted barley may require gentler conveying systems to avoid breakage or damage. Second, the distance and elevation changes between the start and end points of the conveying process are critical. Gravity systems are best for short, level or slightly inclined paths, while mechanical and air systems are more suitable for longer distances or vertical lifts. Third, the overall cost and maintenance requirements of the system must be evaluated. Mechanical systems, such as belt conveyors, may have higher initial costs but lower long-term maintenance compared to air systems, which require regular filter and air compressor maintenance. HeadPowder Engineering assists clients in evaluating these factors and recommending the most suitable conveying solution for their specific needs, ensuring that the chosen system aligns with their operational goals and budget constraints.
Conclusion
Efficient malted barley conveying is essential for maintaining the quality and consistency of the brewing process. Whether using gravity, mechanical, or air conveying systems, the right choice depends on the specific requirements of the facility. Shandong HeadPowder Engineering Co., Ltd. offers a range of specialized conveying solutions tailored to the needs of the malted barley industry, ensuring reliable and efficient material handling. By understanding the different methods and their applications, breweries can optimize their operations and enhance overall productivity.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu