Với hơn 10 năm kinh nghiệm về vận chuyển khí nén, Headpowder Sơn Đông cung cấp hệ thống, thiết bị và quạt gió toàn chuỗi, đảm nhận các dự án kỹ thuật bột trọn gói trên toàn quốc.
Ammonium bicarbonate, a critical chemical widely used in fertilizer production, pharmaceuticals, and food processing, presents unique challenges during transportation due to its hygroscopic nature and tendency to caking. Traditional methods like belt conveyors or manual handling often fall short in maintaining product quality and efficiency. This article explores effective transportation solutions, with a focus on HeadPowder's advanced pneumatic conveying system designed specifically for ammonium bicarbonate.
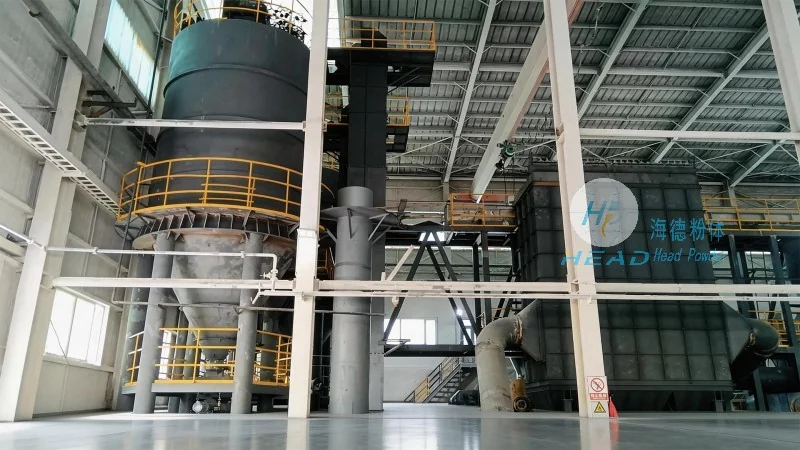
HeadPowder's Pneumatic Conveying System for Ammonium Bicarbonate
Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions, has developed a specialized pneumatic conveying system tailored to the demands of ammonium bicarbonate. The system leverages positive pressure or negative pressure air flow to transport the material from storage silos to processing units, ensuring minimal product degradation and operational efficiency. HeadPowder's expertise in material flow dynamics and system integration ensures that the conveying process is optimized for both safety and performance.
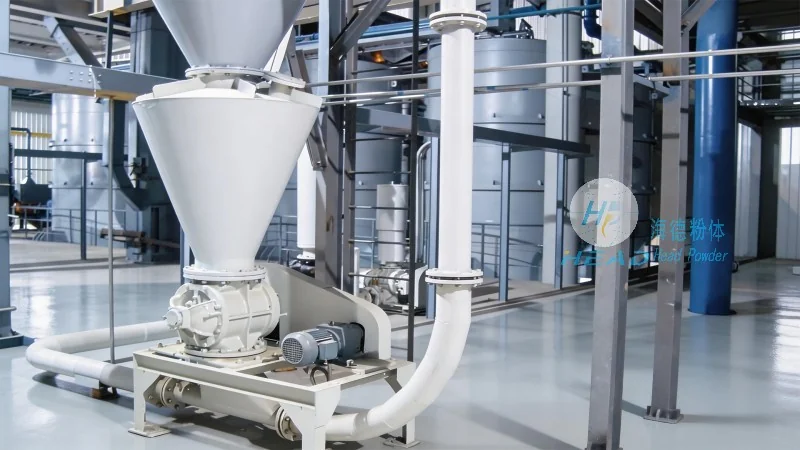
Key Features and Advantages of the Pneumatic Conveying Solution
The pneumatic conveying system from HeadPowder offers several key advantages that address the challenges of ammonium bicarbonate transportation. Firstly, it maintains a consistent product temperature and moisture level, preventing caking and clumping during transit. Secondly, the system operates with minimal human intervention, reducing labor costs and improving safety in industrial environments. Additionally, the enclosed conveying process minimizes dust emissions, aligning with environmental regulations and enhancing workplace safety. The modular design of the system allows for easy installation and scalability, making it suitable for both small-scale and large-scale production facilities.
Application Scenarios and Operational Benefits
HeadPowder's ammonium bicarbonate pneumatic conveying system is applicable in various industrial settings, including fertilizer manufacturing plants, chemical processing facilities, and food processing industries. In fertilizer production, the system efficiently transfers ammonium bicarbonate from storage to mixing and granulation units, ensuring a steady supply of raw material. In pharmaceutical applications, the enclosed conveying process maintains product purity and sterility, meeting stringent quality standards. The operational benefits extend to reduced downtime, as the system's robust design minimizes maintenance requirements and ensures continuous operation. Furthermore, the energy-efficient design of the system contributes to lower operational costs, making it a cost-effective solution for long-term use.
Technical Specifications and System Components
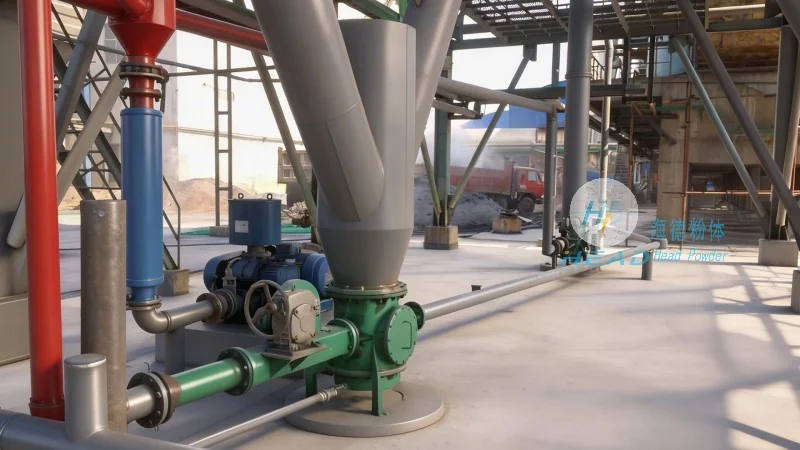
HeadPowder's pneumatic conveying system for ammonium bicarbonate is equipped with advanced components that enhance its performance and reliability. The system includes high-quality air blowers, dust filters, and material feeders designed to handle the hygroscopic properties of ammonium bicarbonate. The air blowers are selected based on the required flow rate and pressure, ensuring optimal material transport. The dust filters are equipped with efficient filtration media that capture fine particles, preventing contamination and maintaining air quality. The material feeders are designed with anti-caking mechanisms, such as vibration or agitation, to prevent material buildup and ensure smooth flow. The system also features pressure sensors and flow meters that provide real-time monitoring of the conveying process, allowing for immediate adjustments if any issues arise.
Conclusion and Contact Information
HeadPowder's pneumatic conveying system represents a superior solution for ammonium bicarbonate transportation, addressing the unique challenges associated with this material. By leveraging advanced technology and engineering expertise, HeadPowder ensures that the system meets the highest standards of efficiency, safety, and reliability. For businesses seeking to optimize their ammonium bicarbonate handling processes, HeadPowder offers tailored solutions that enhance productivity and product quality. Shandong HeadPowder Engineering Co., Ltd., based in China, provides comprehensive support and customization to meet the specific needs of each client. Contact HeadPowder today to learn more about their pneumatic conveying solutions for ammonium bicarbonate.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu